PE Christmas Tree Branch Painting Machine
Dual Level 4 Output
Centre-stem painting on upper and lower levels.
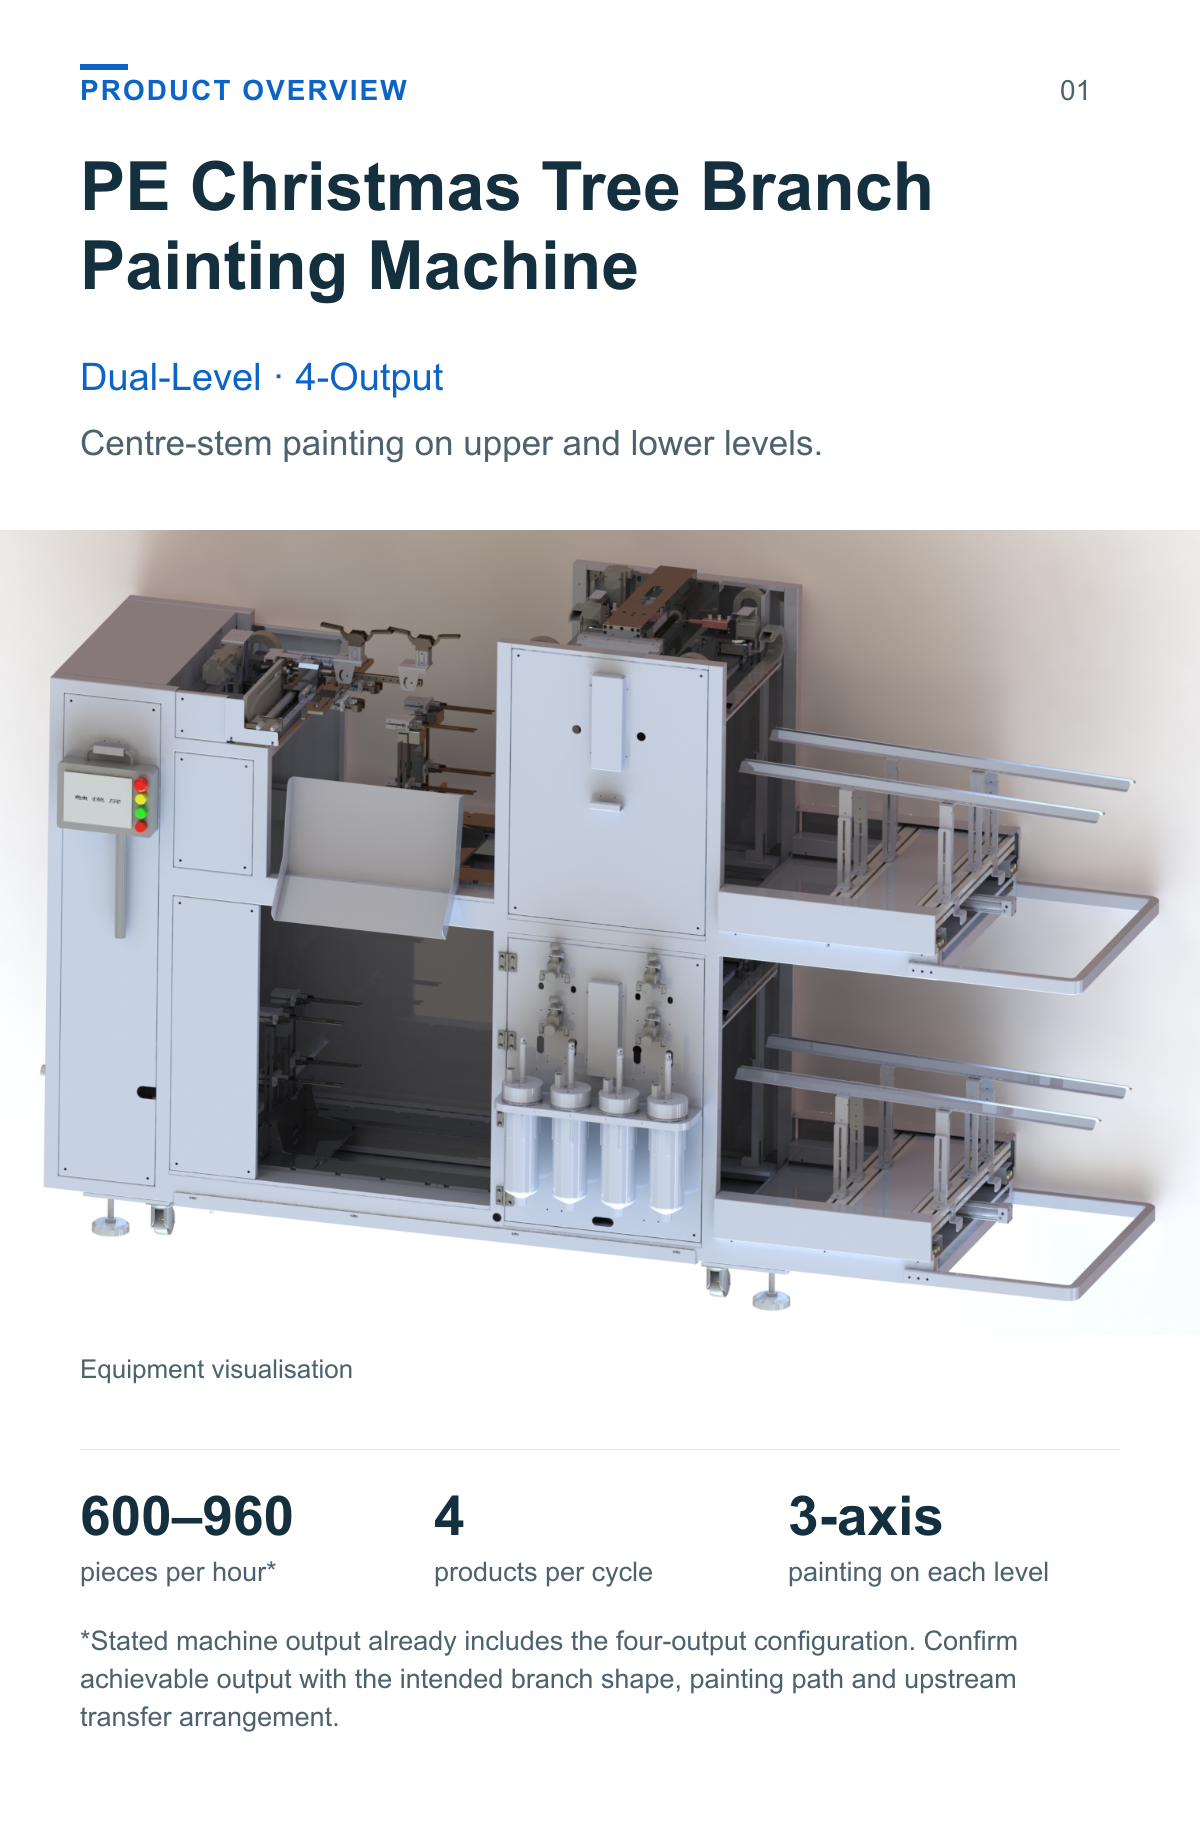
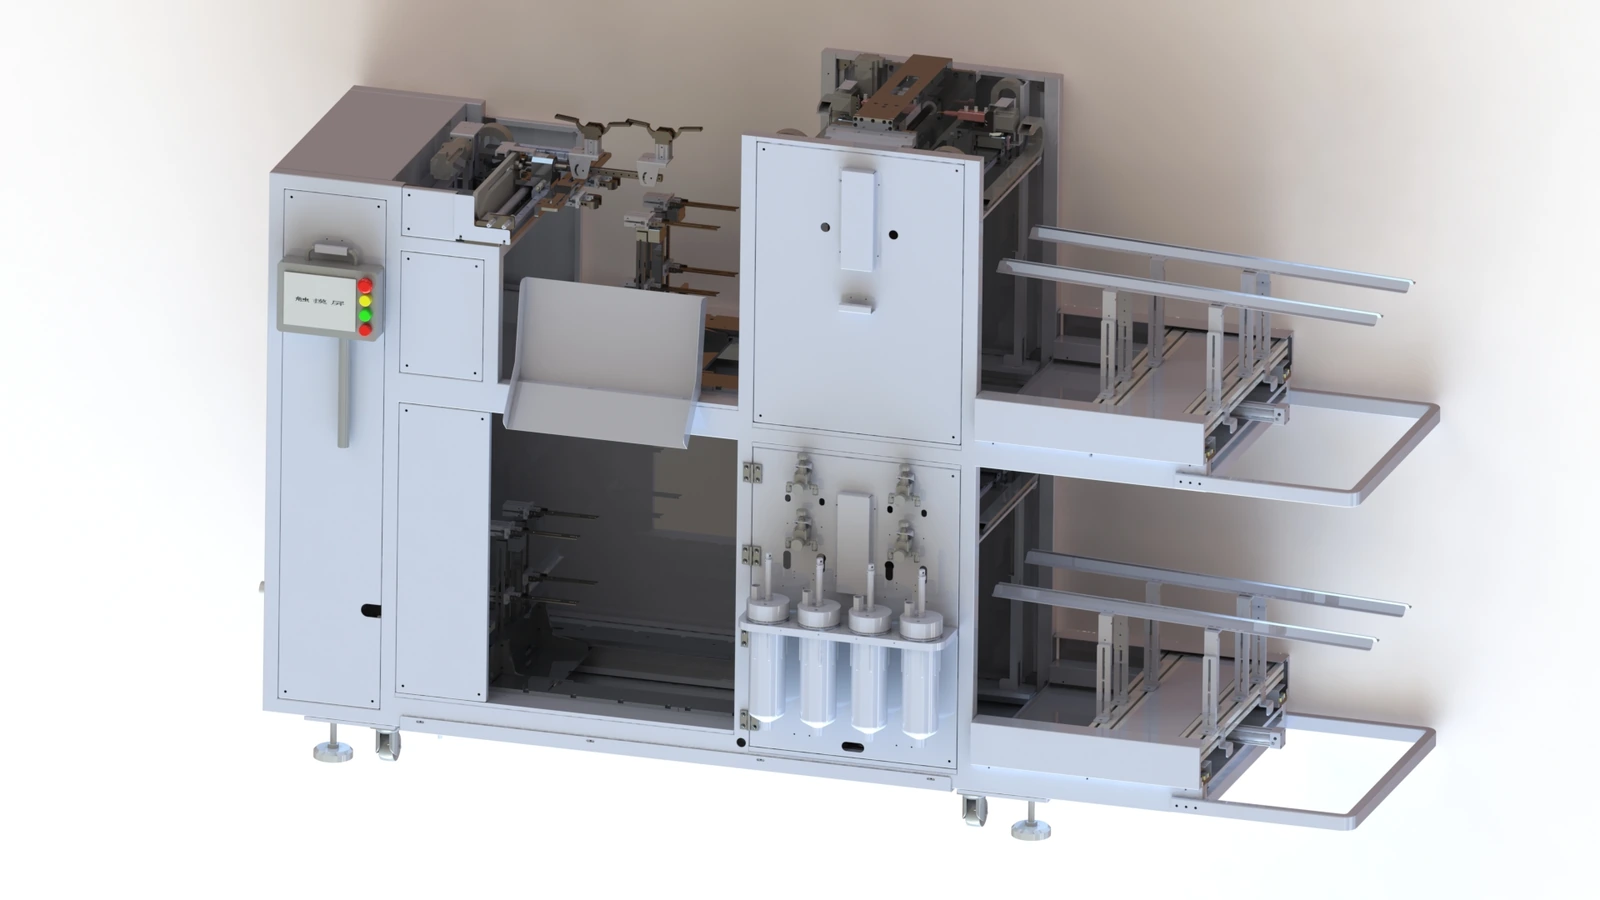
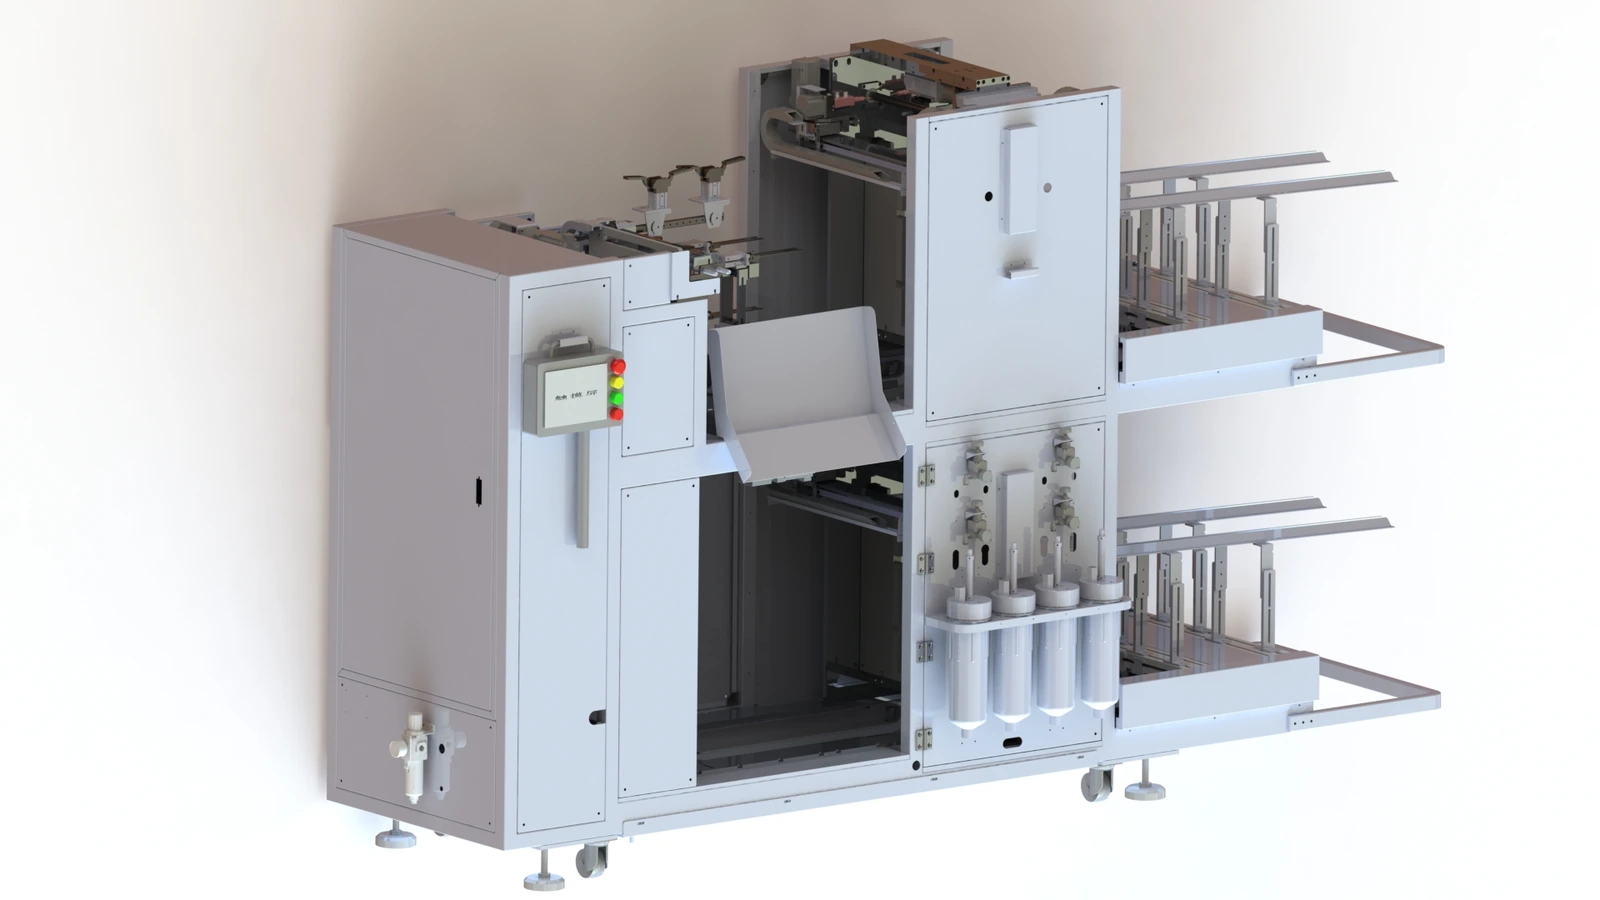
This dual-level, 4-output yellow core painting machine receives moulded PE branches from an upstream robot. Upper and lower receiving assemblies, painting units and product racks support the documented receive, position, paint and place cycle.
600–960 pieces per hour*
4 products per cycle
3-axis painting on each level
*Stated machine output already includes the four-output configuration. Confirm achievable output with the intended branch shape, painting path and upstream transfer arrangement.
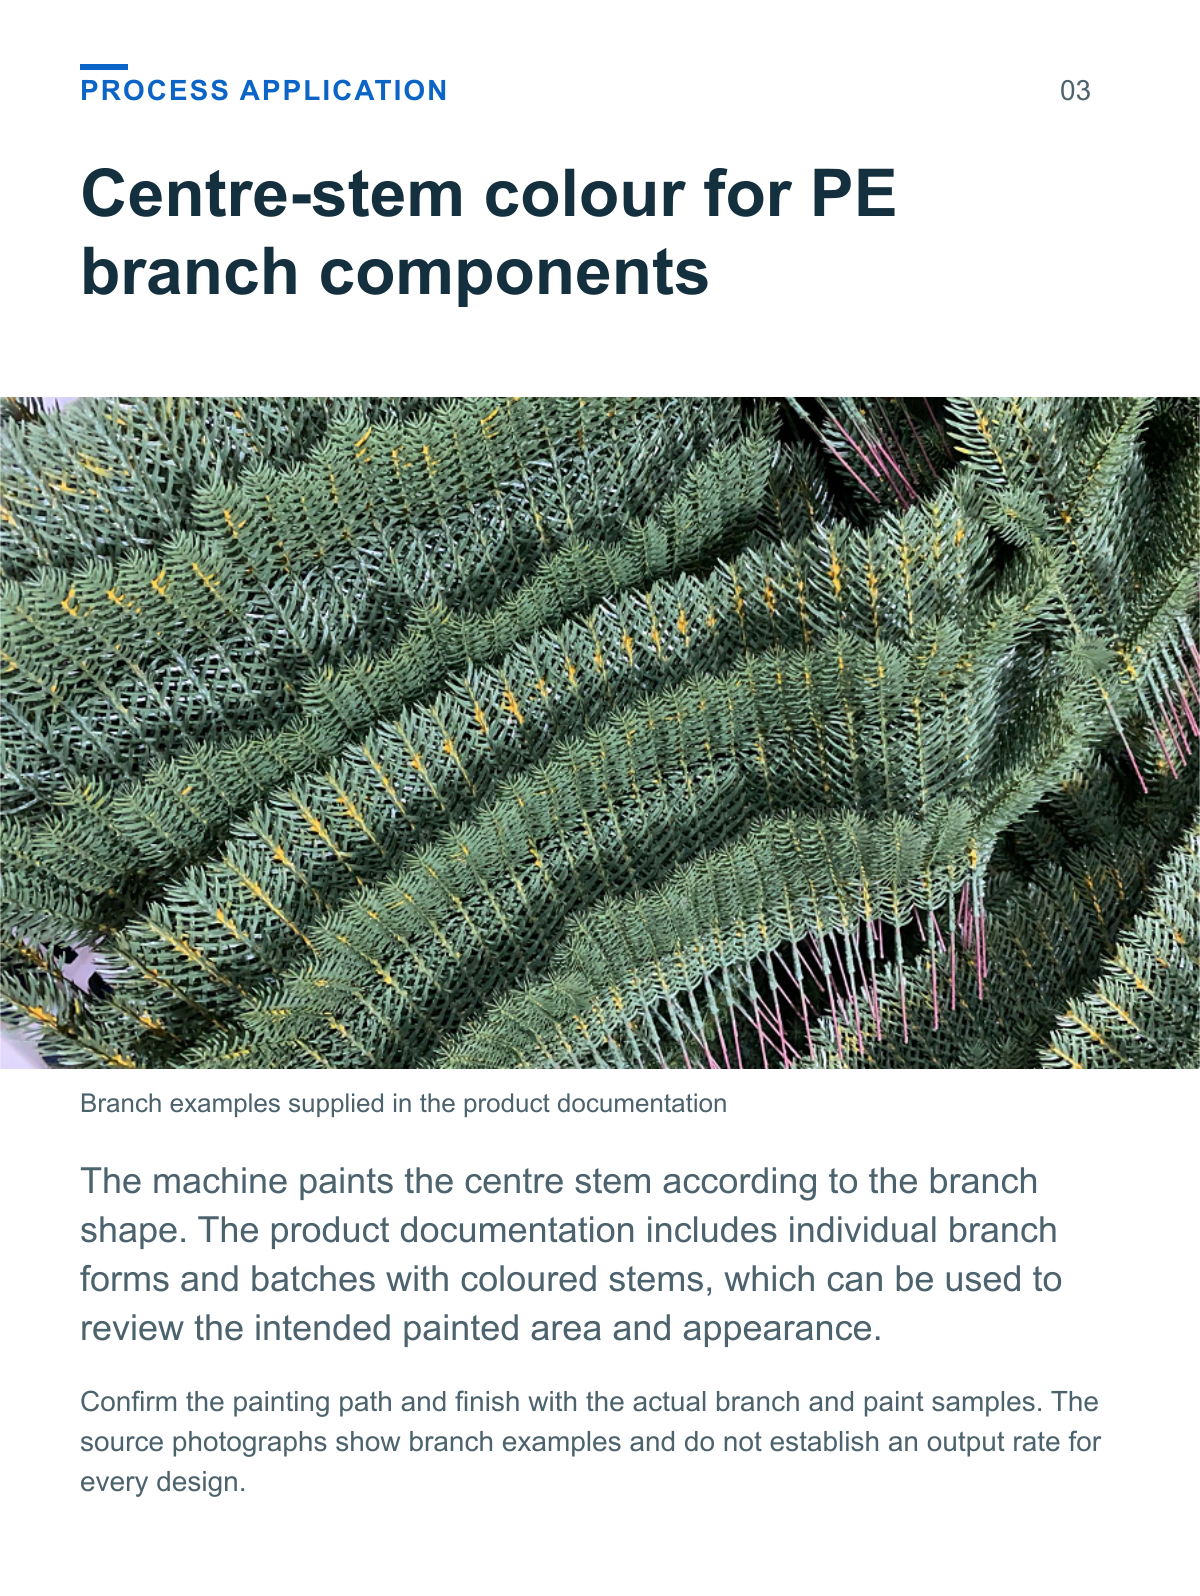
Centre stem colour for PE branch components
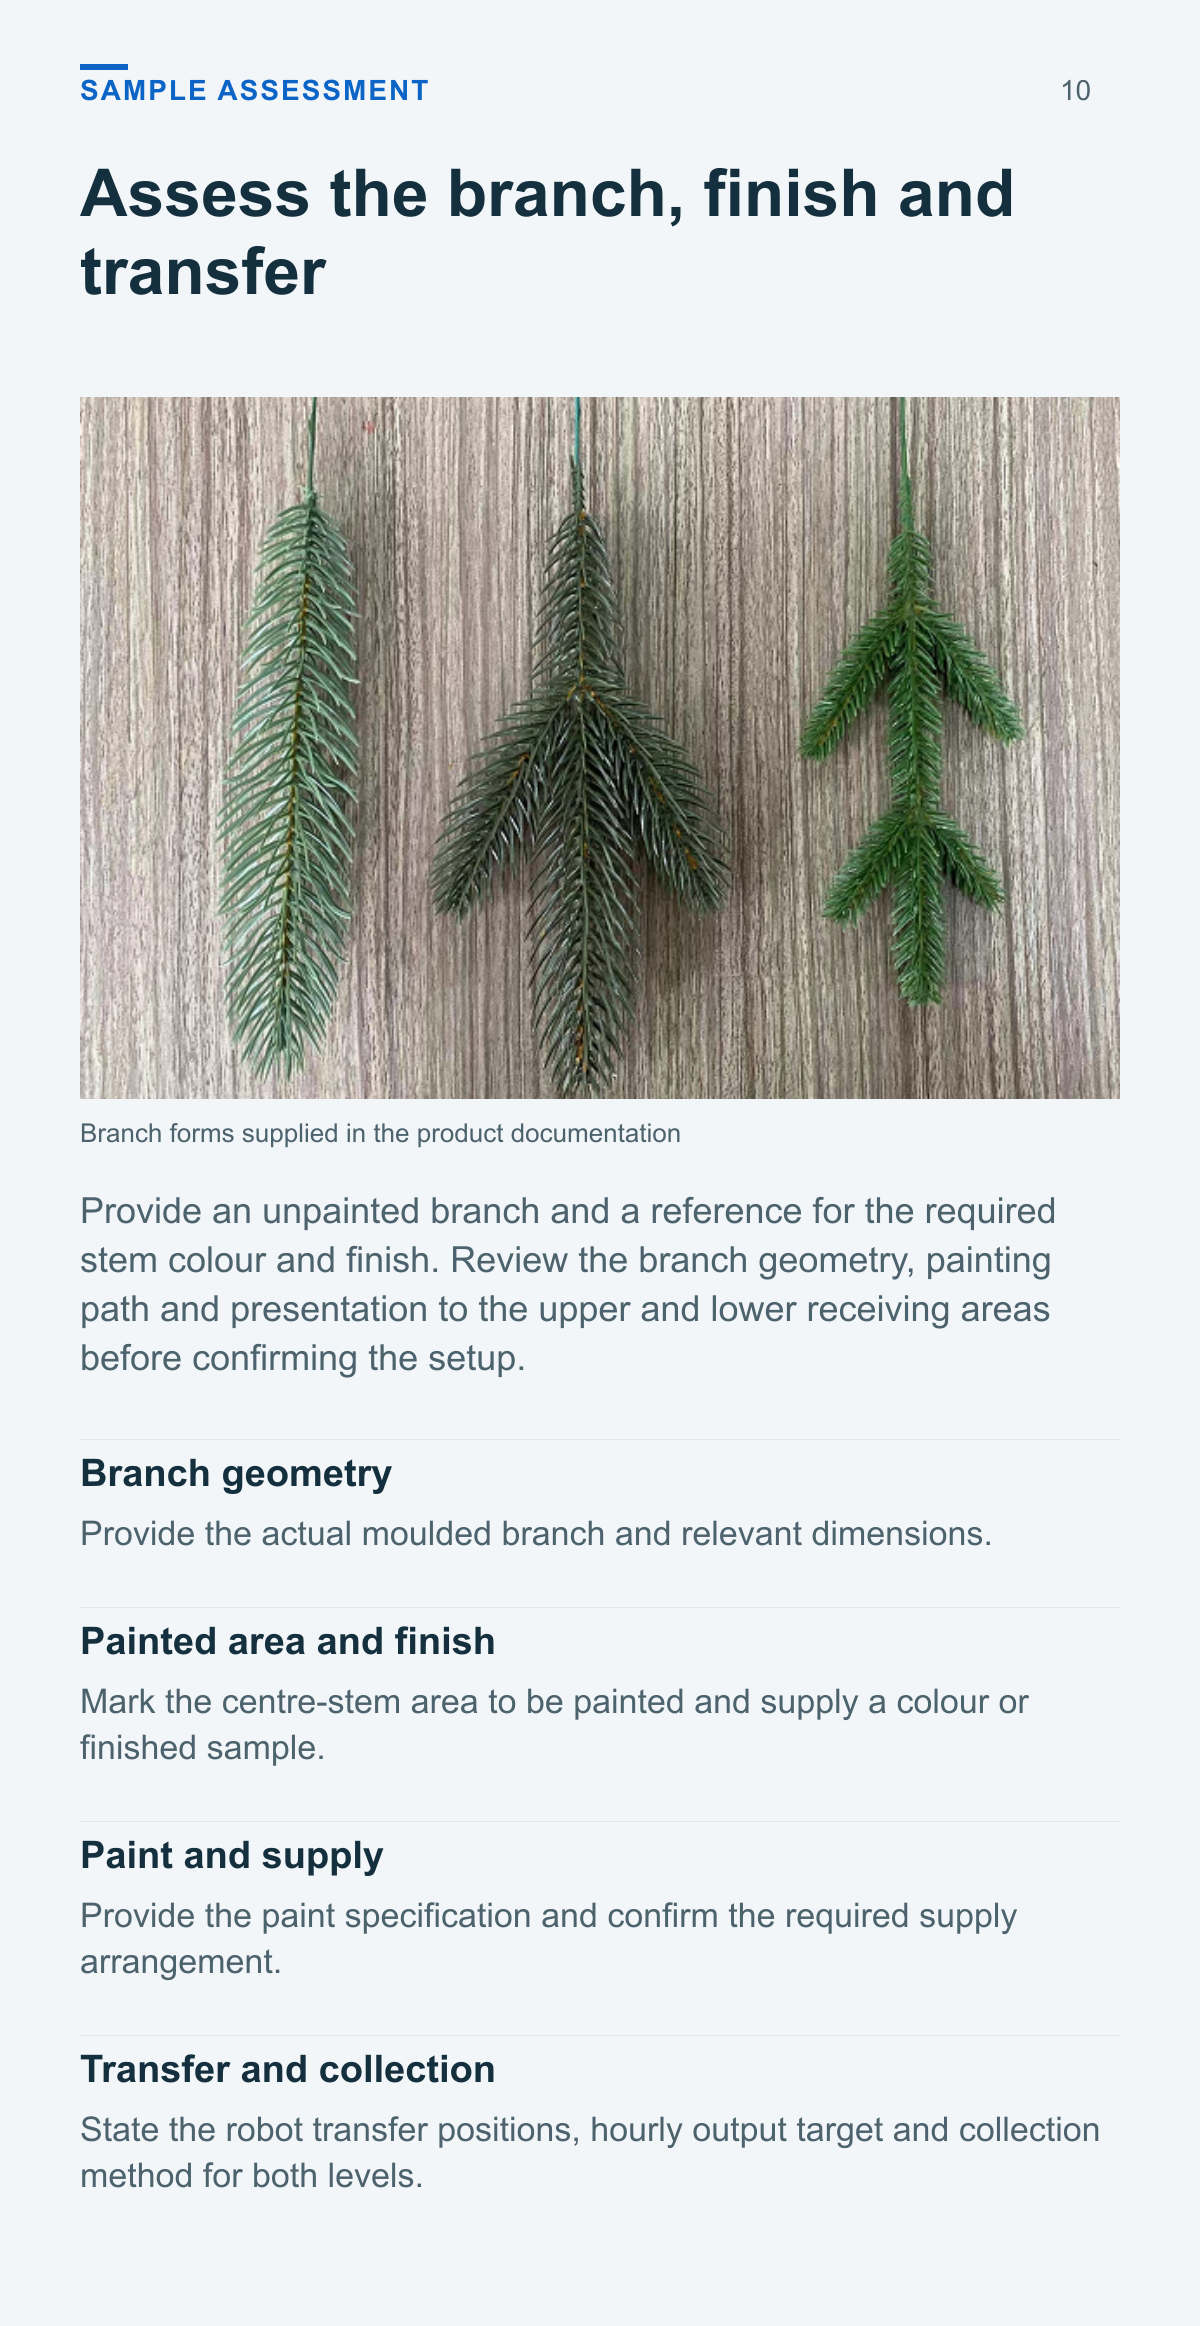
The machine paints the centre stem according to the branch shape. The product documentation includes individual branch forms and batches with coloured stems, which can be used to review the intended painted area and appearance.
Receive position paint and place
The documented process repeats four stages. The dual-level layout has receiving assemblies, painting structures and product racks on both the upper and lower levels.
Receive the branches Upper and lower receiving assemblies accept products from the upstream robot.
Position for painting The branches are positioned before centre-stem painting.
Paint the centre stems The upper and lower painting units each have three axes and apply colour according to the branch shape.
Place the products Painted branches are placed on the product racks, and the documented cycle repeats.
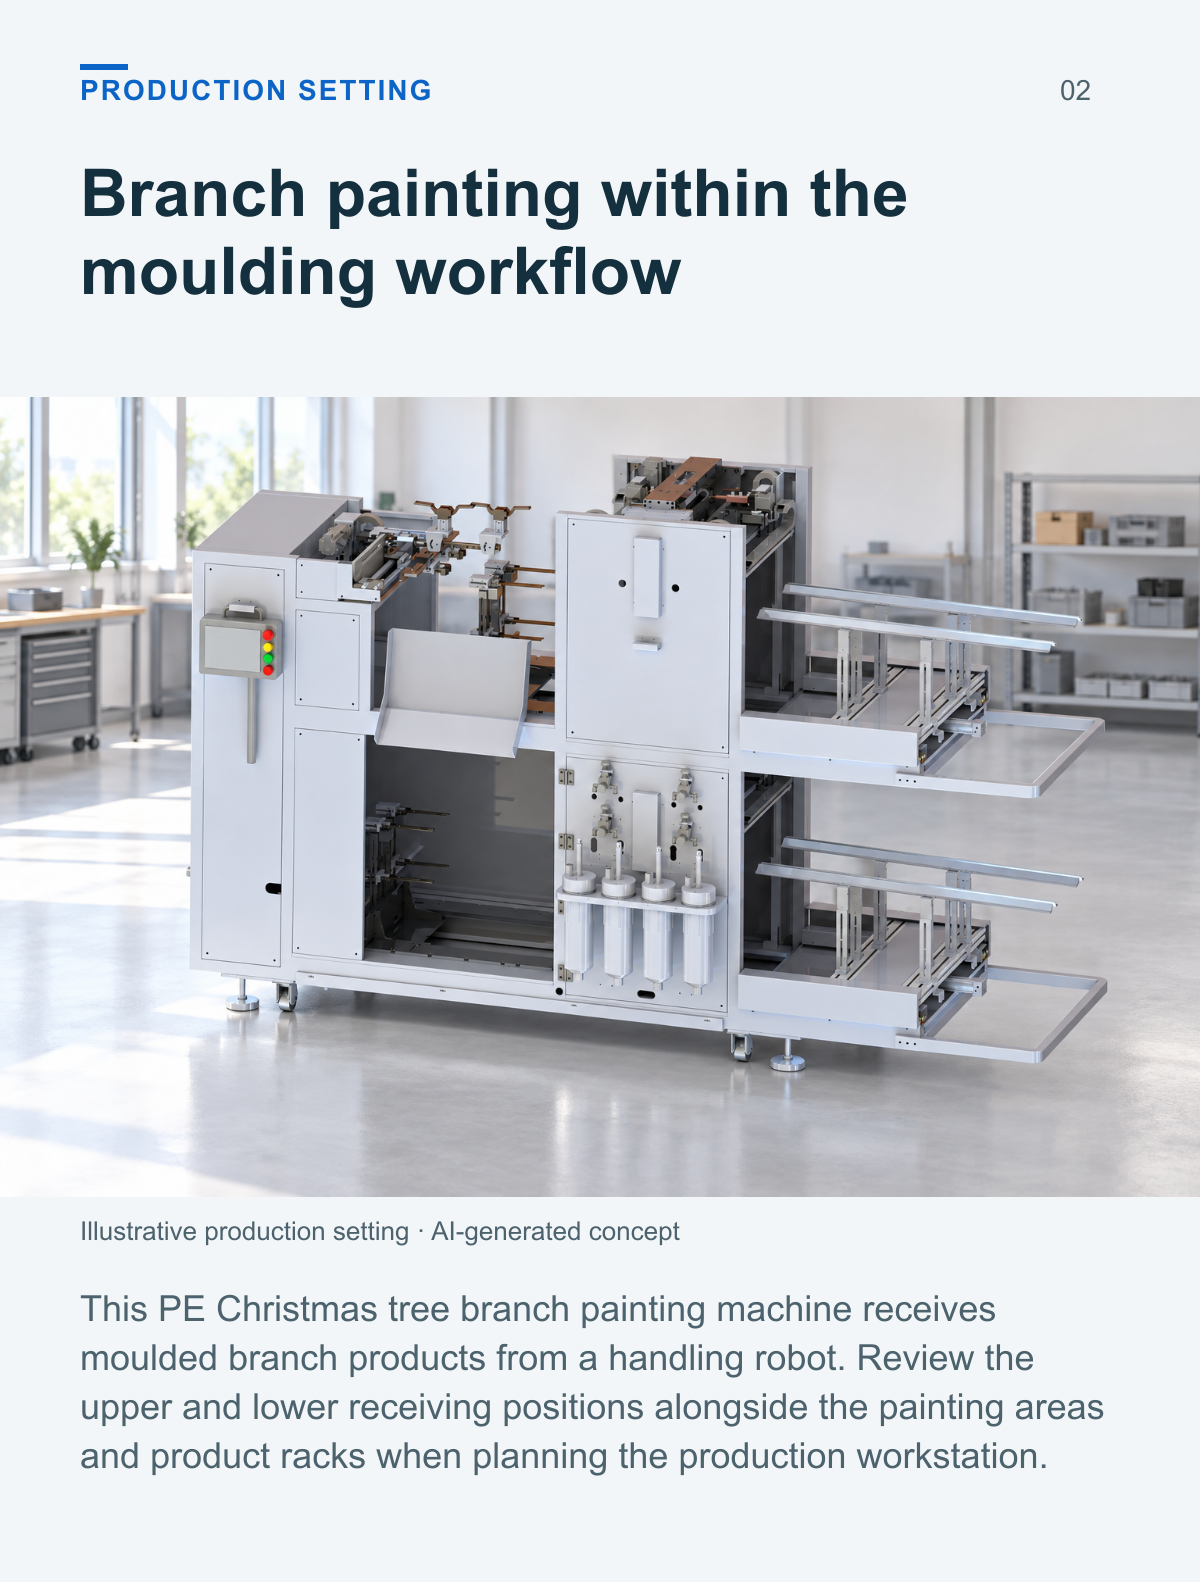
Branch painting within the moulding workflow
This PE Christmas tree branch painting machine receives moulded branch products from a handling robot. Review the upper and lower receiving positions alongside the painting areas and product racks when planning the production workstation.
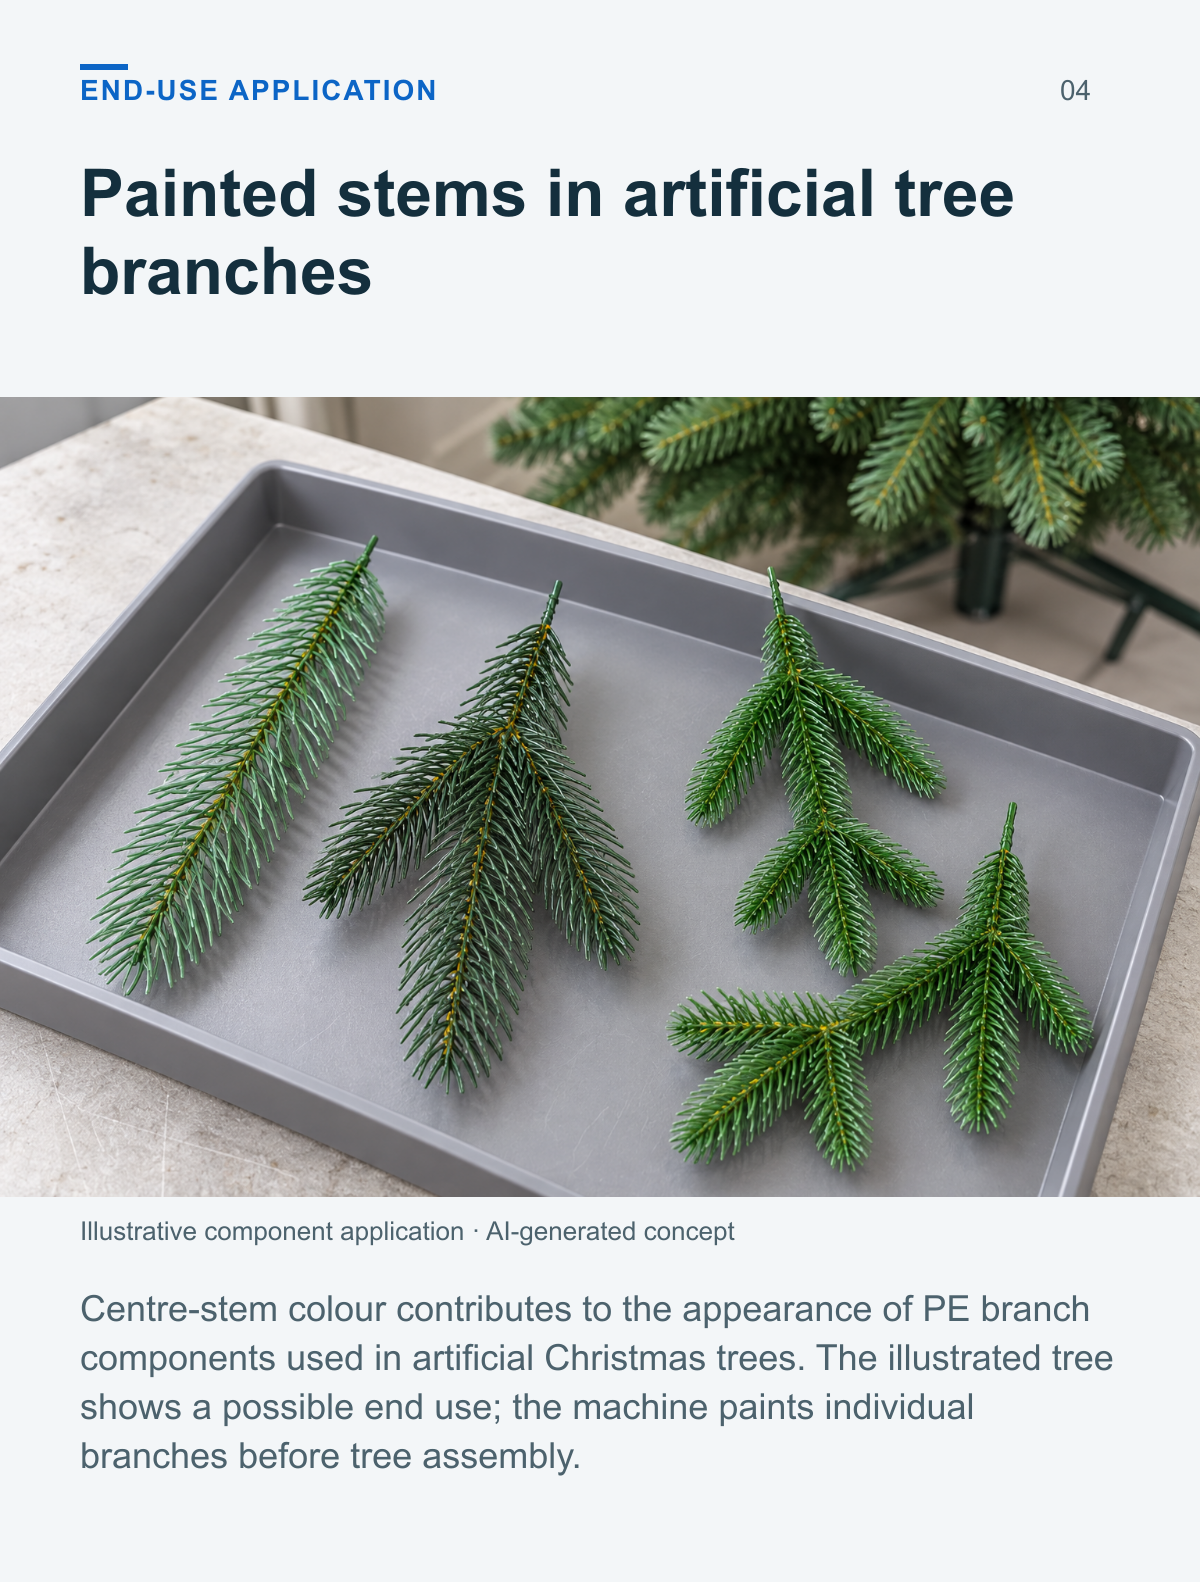
Painted stems in artificial tree branches
Centre-stem colour contributes to the appearance of PE branch components used in artificial Christmas trees. The illustrated tree shows a possible end use; the machine paints individual branches before tree assembly.
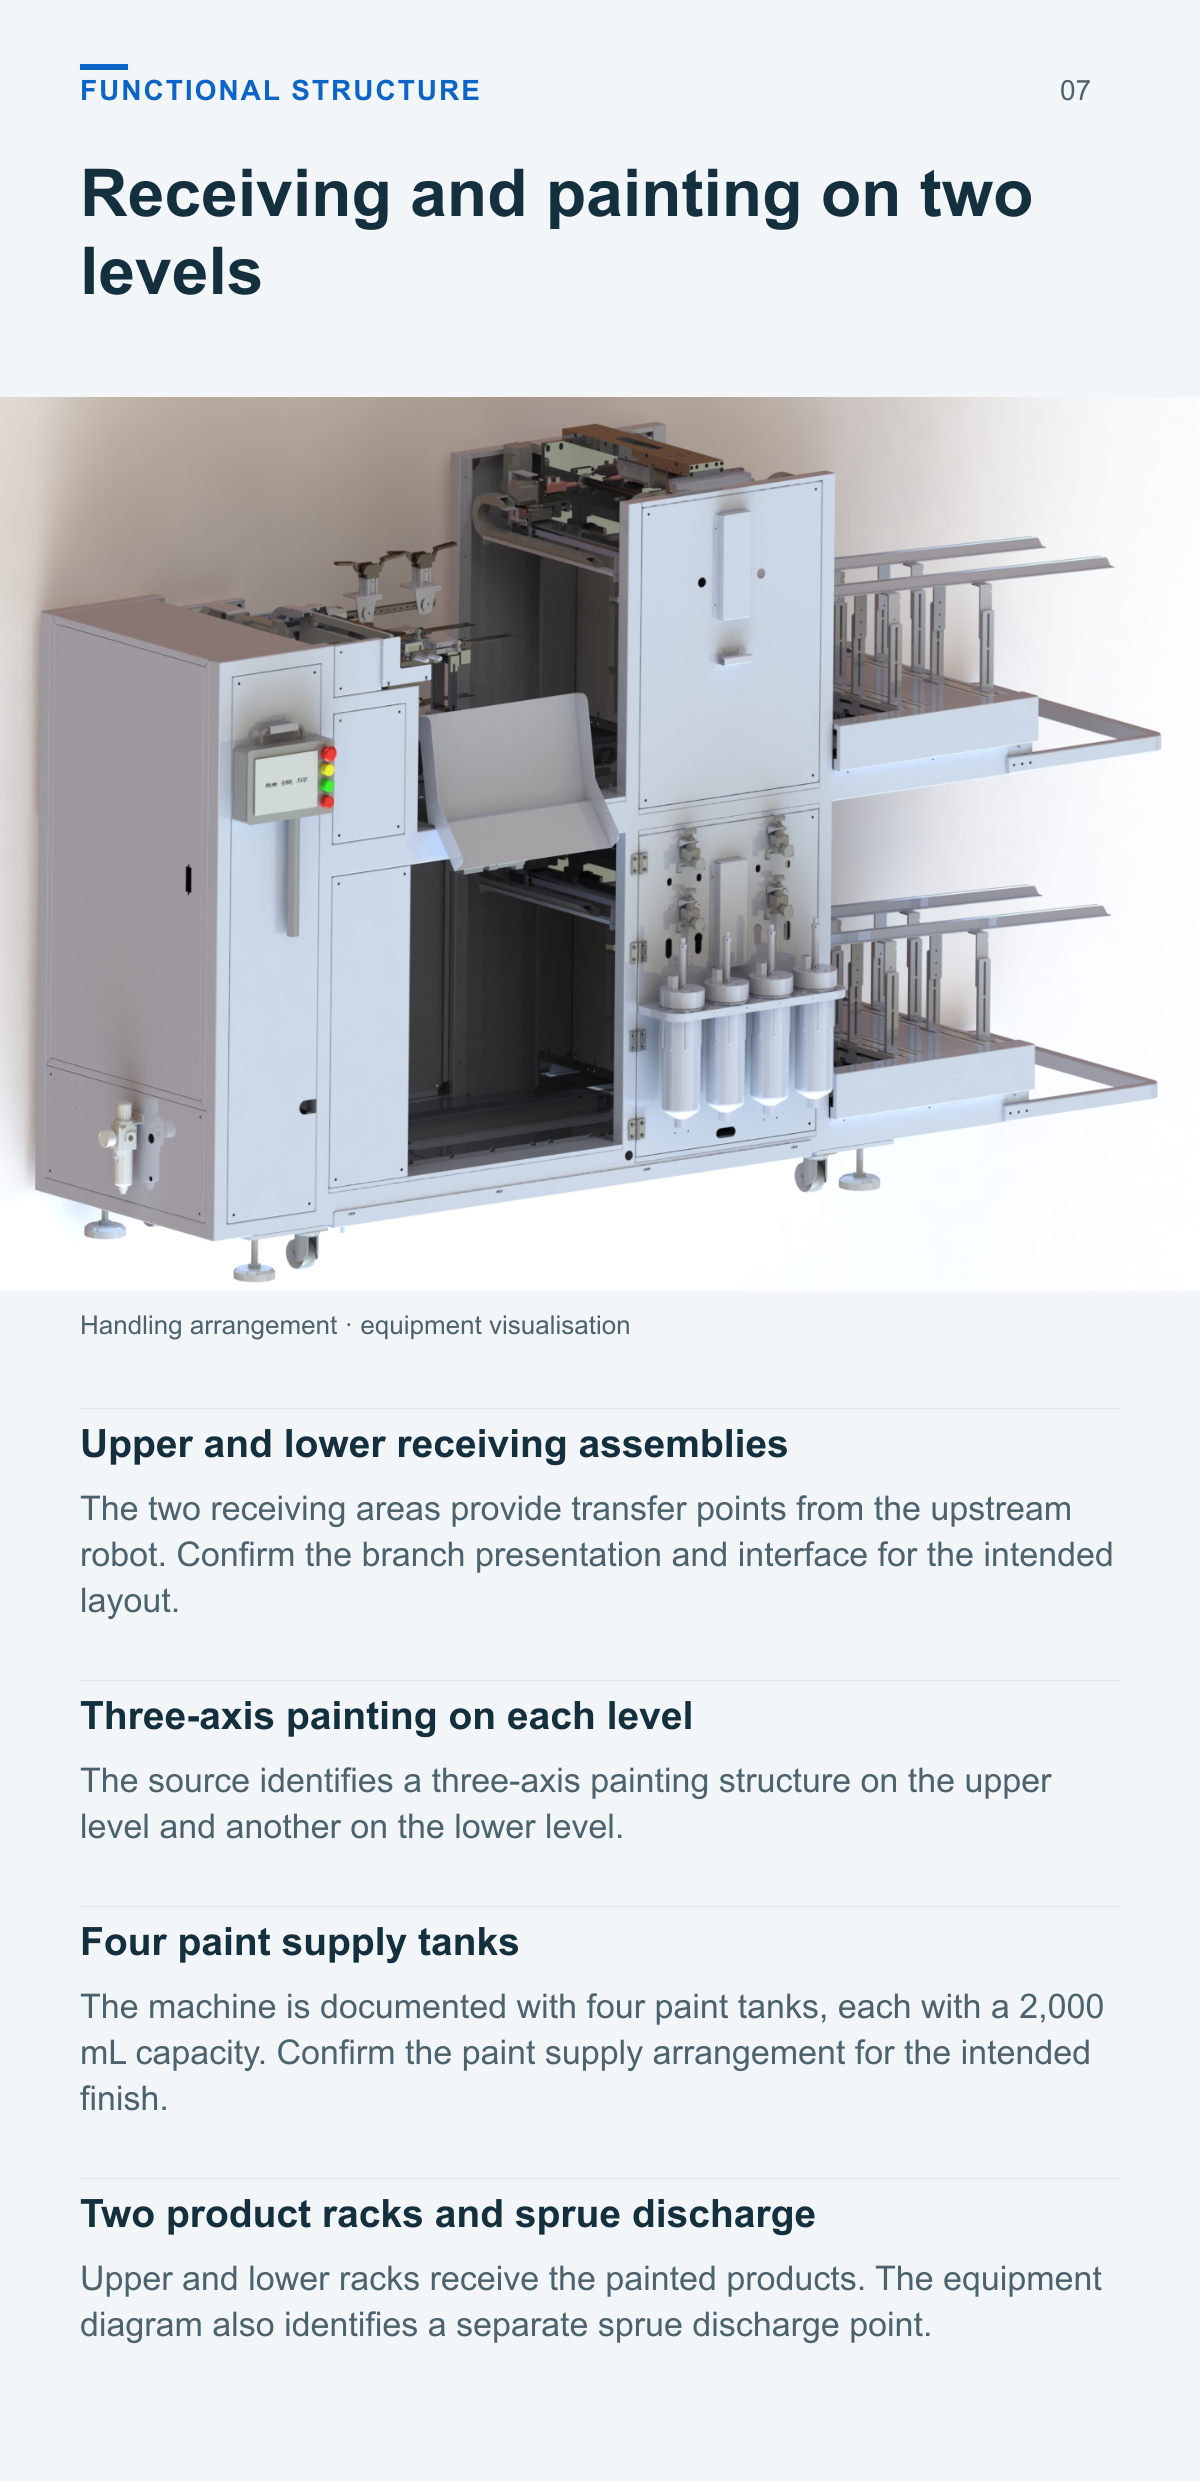
Receiving and painting on two levels
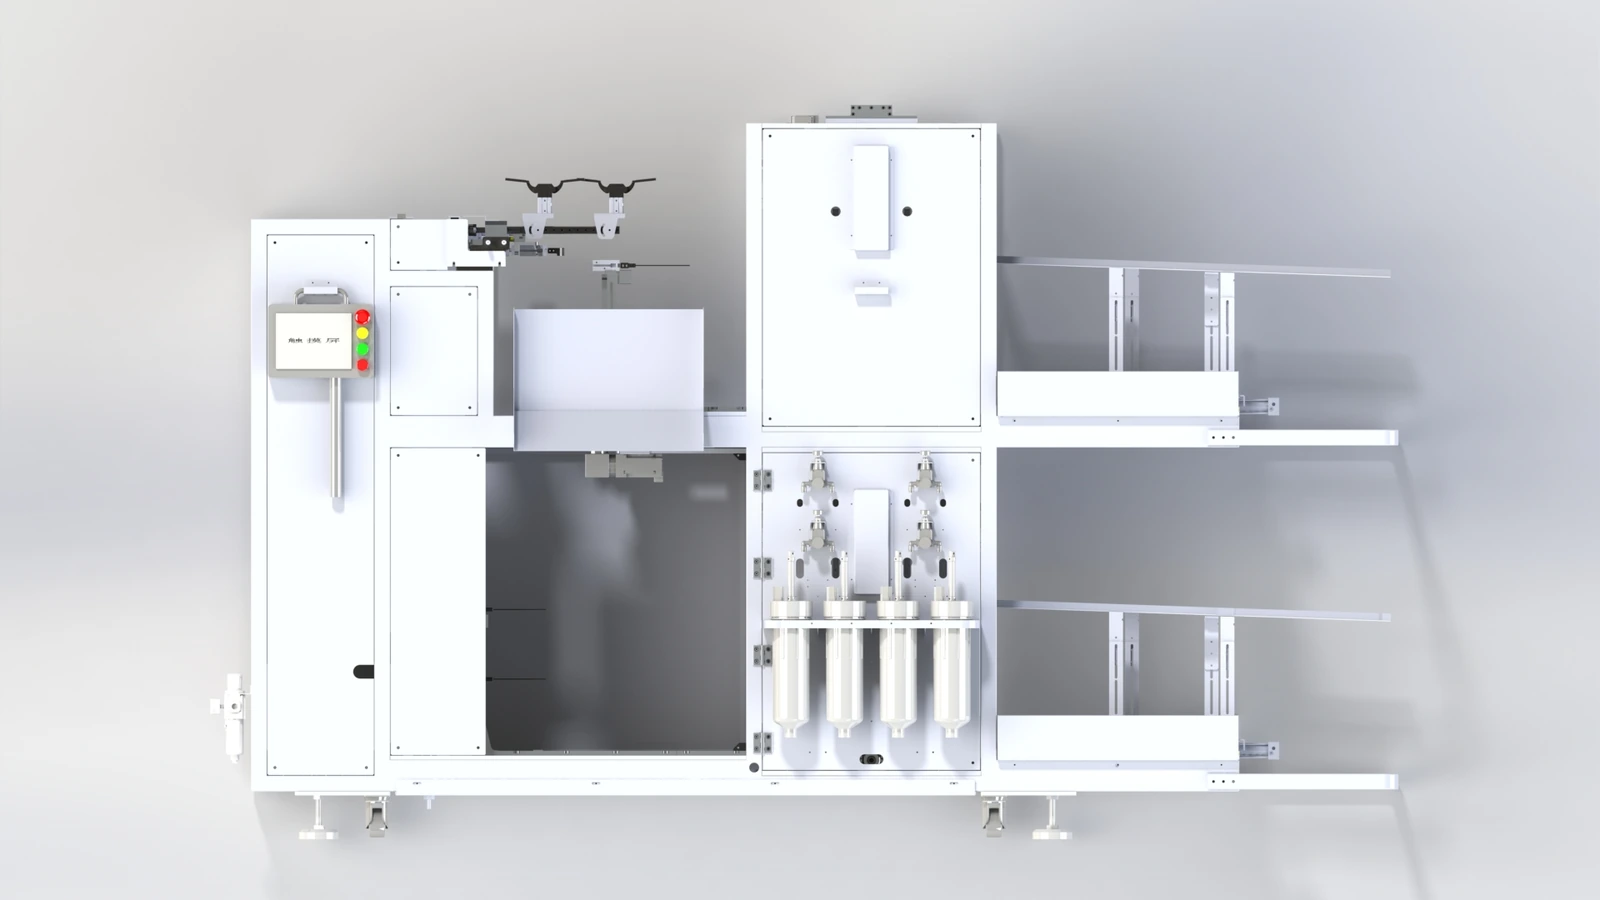
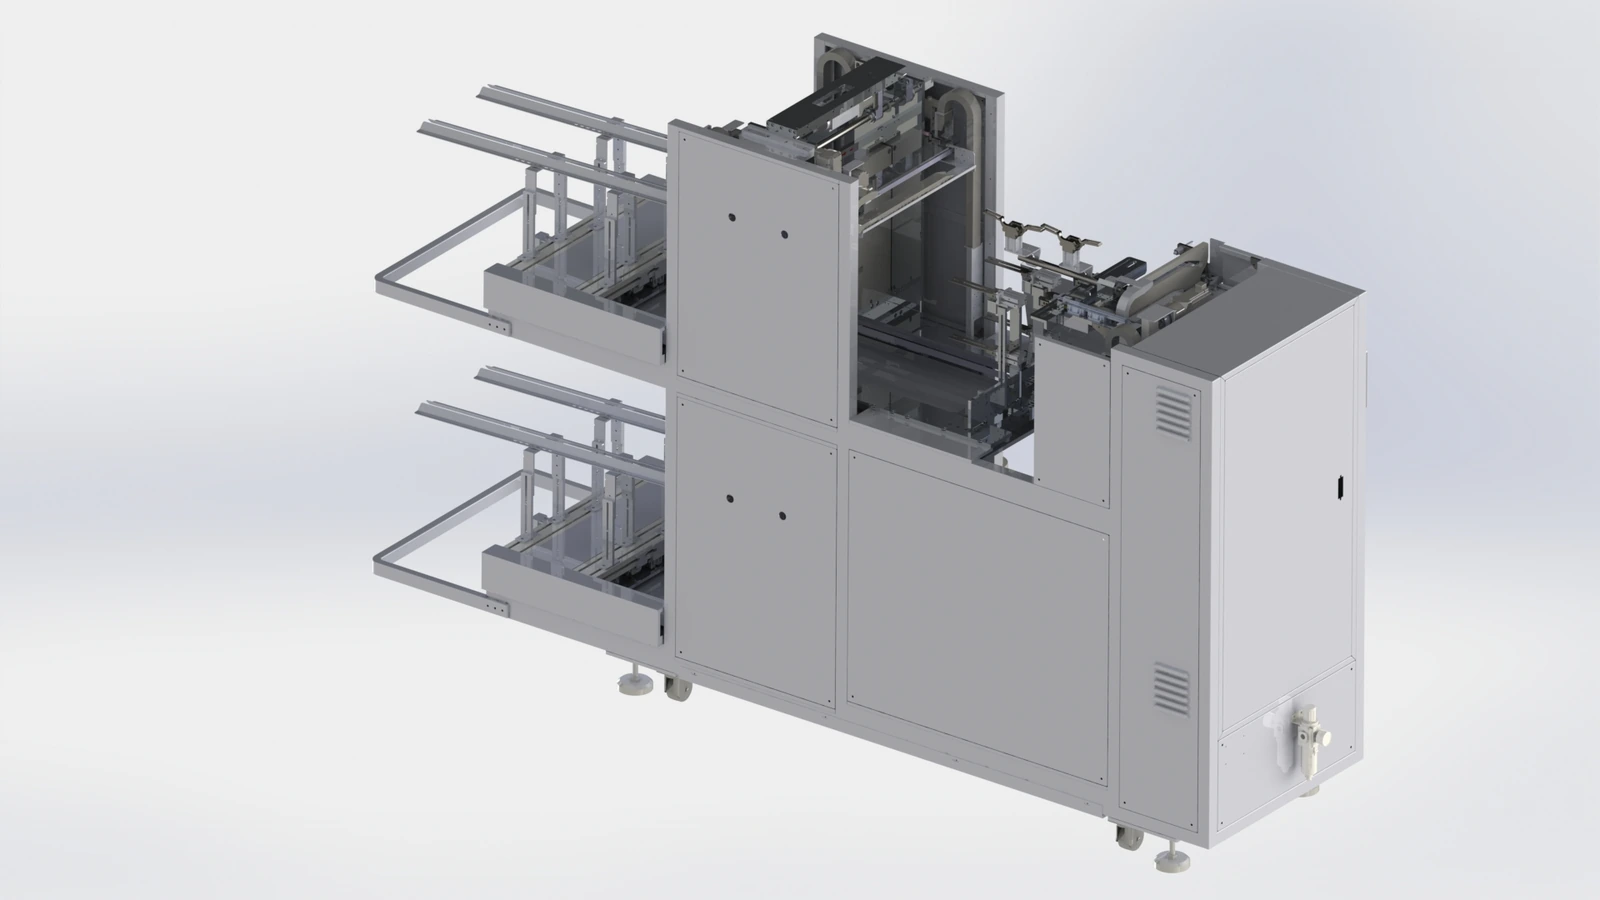
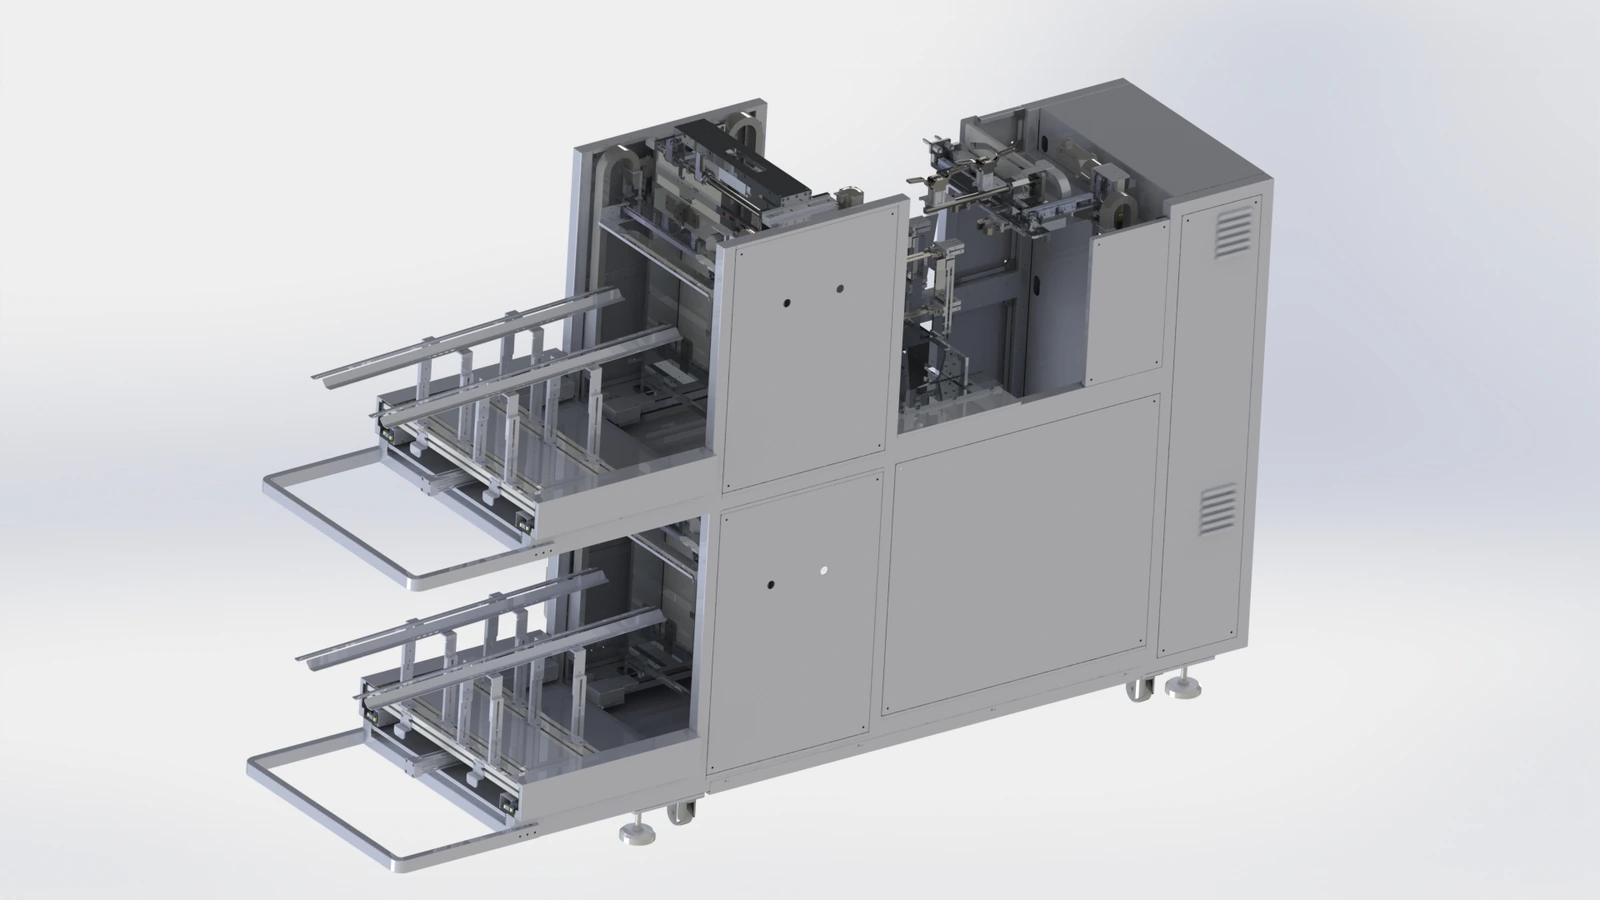
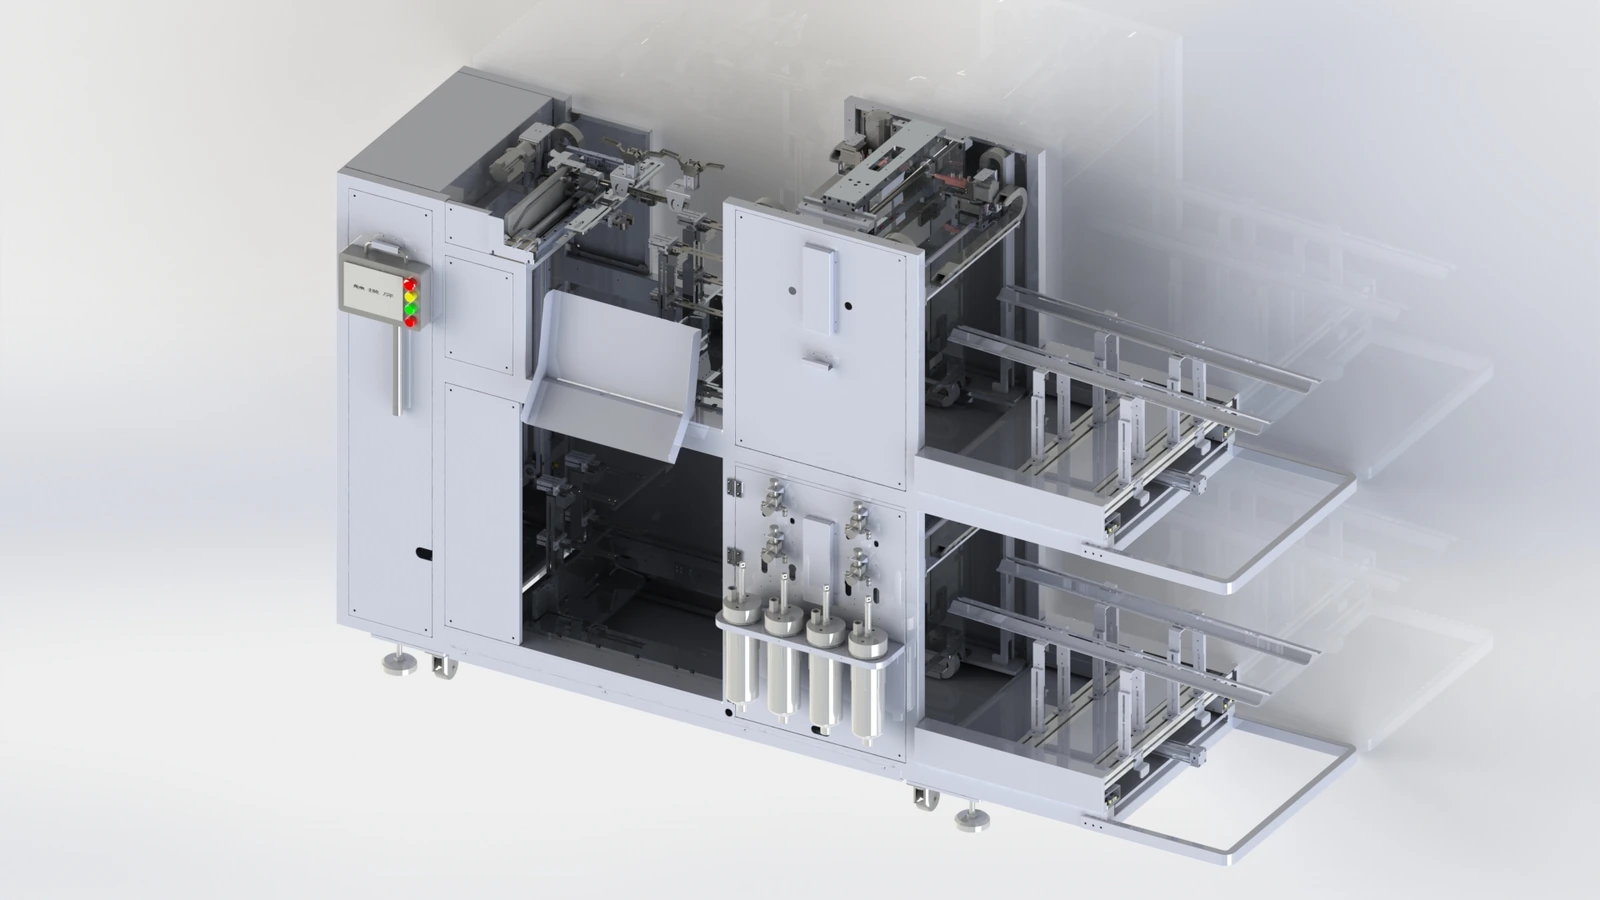
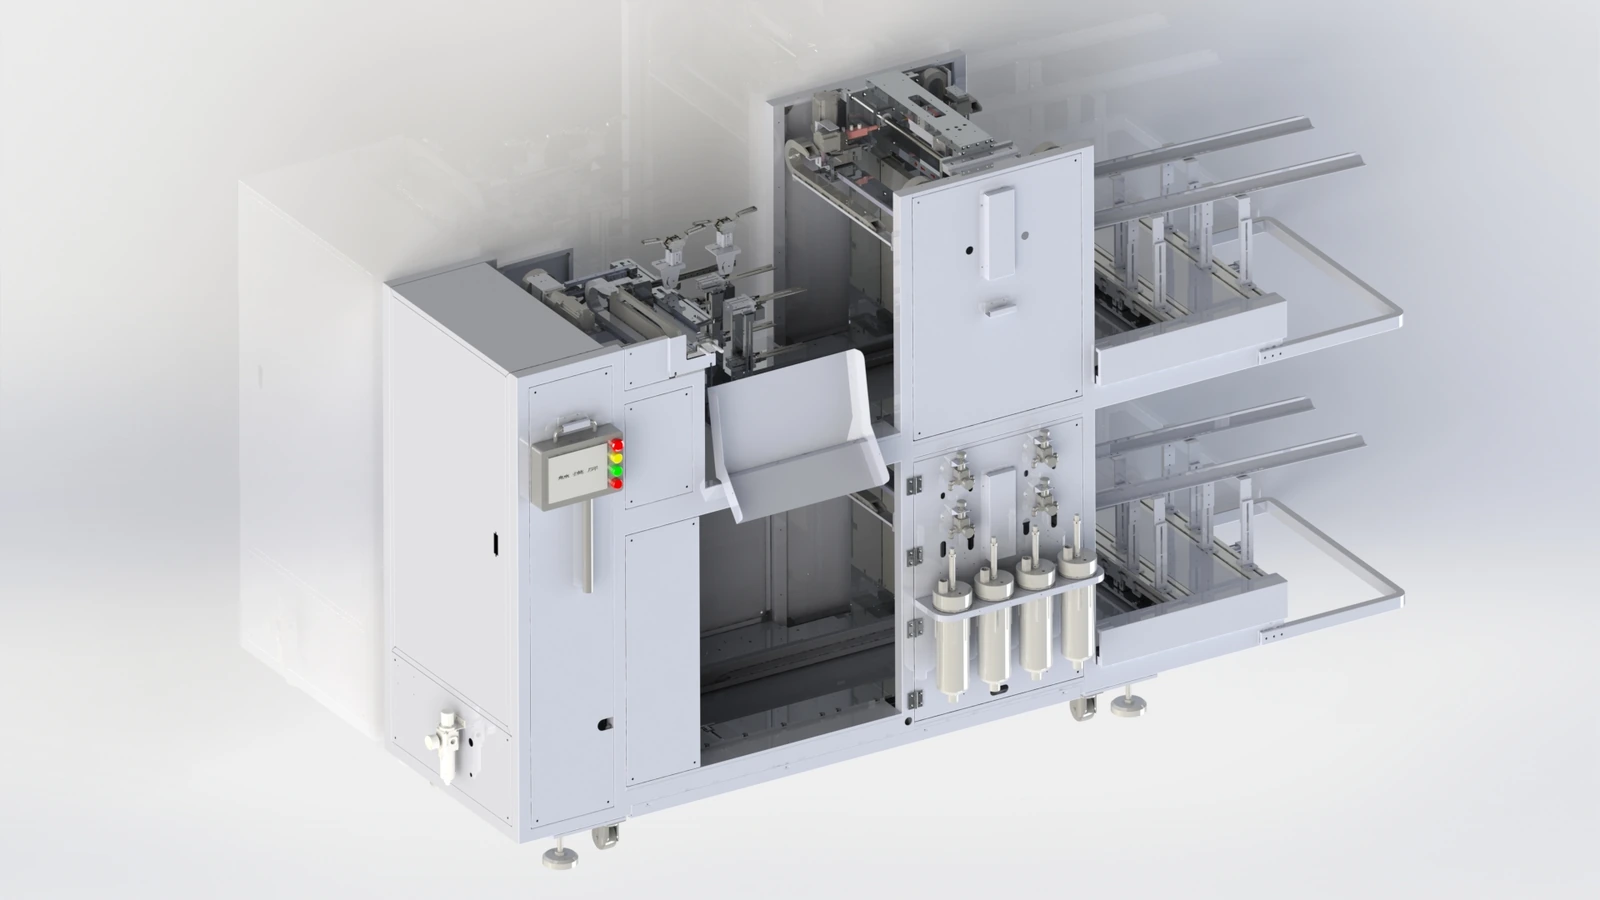
Upper and lower receiving assemblies
The two receiving areas provide transfer points from the upstream robot. Confirm the branch presentation and interface for the intended layout.
Three axis painting on each level
The source identifies a three-axis painting structure on the upper level and another on the lower level.
Four paint supply tanks
The machine is documented with four paint tanks, each with a 2,000 mL capacity. Confirm the paint supply arrangement for the intended finish.
Two product racks and sprue discharge
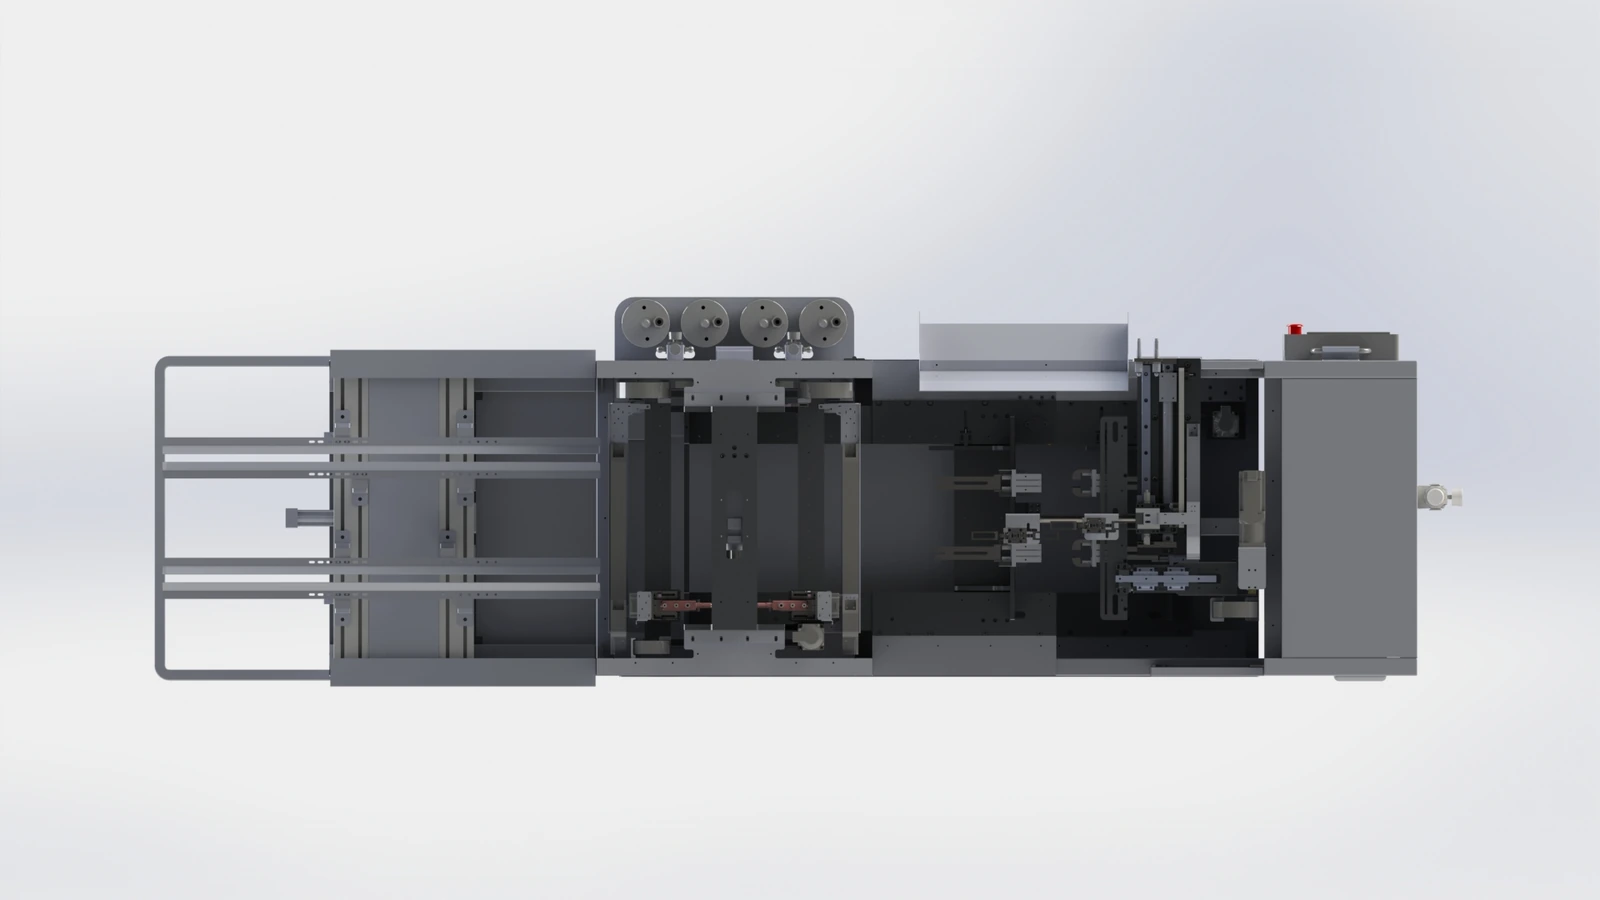
Upper and lower racks receive the painted products. The equipment diagram also identifies a separate sprue discharge point.
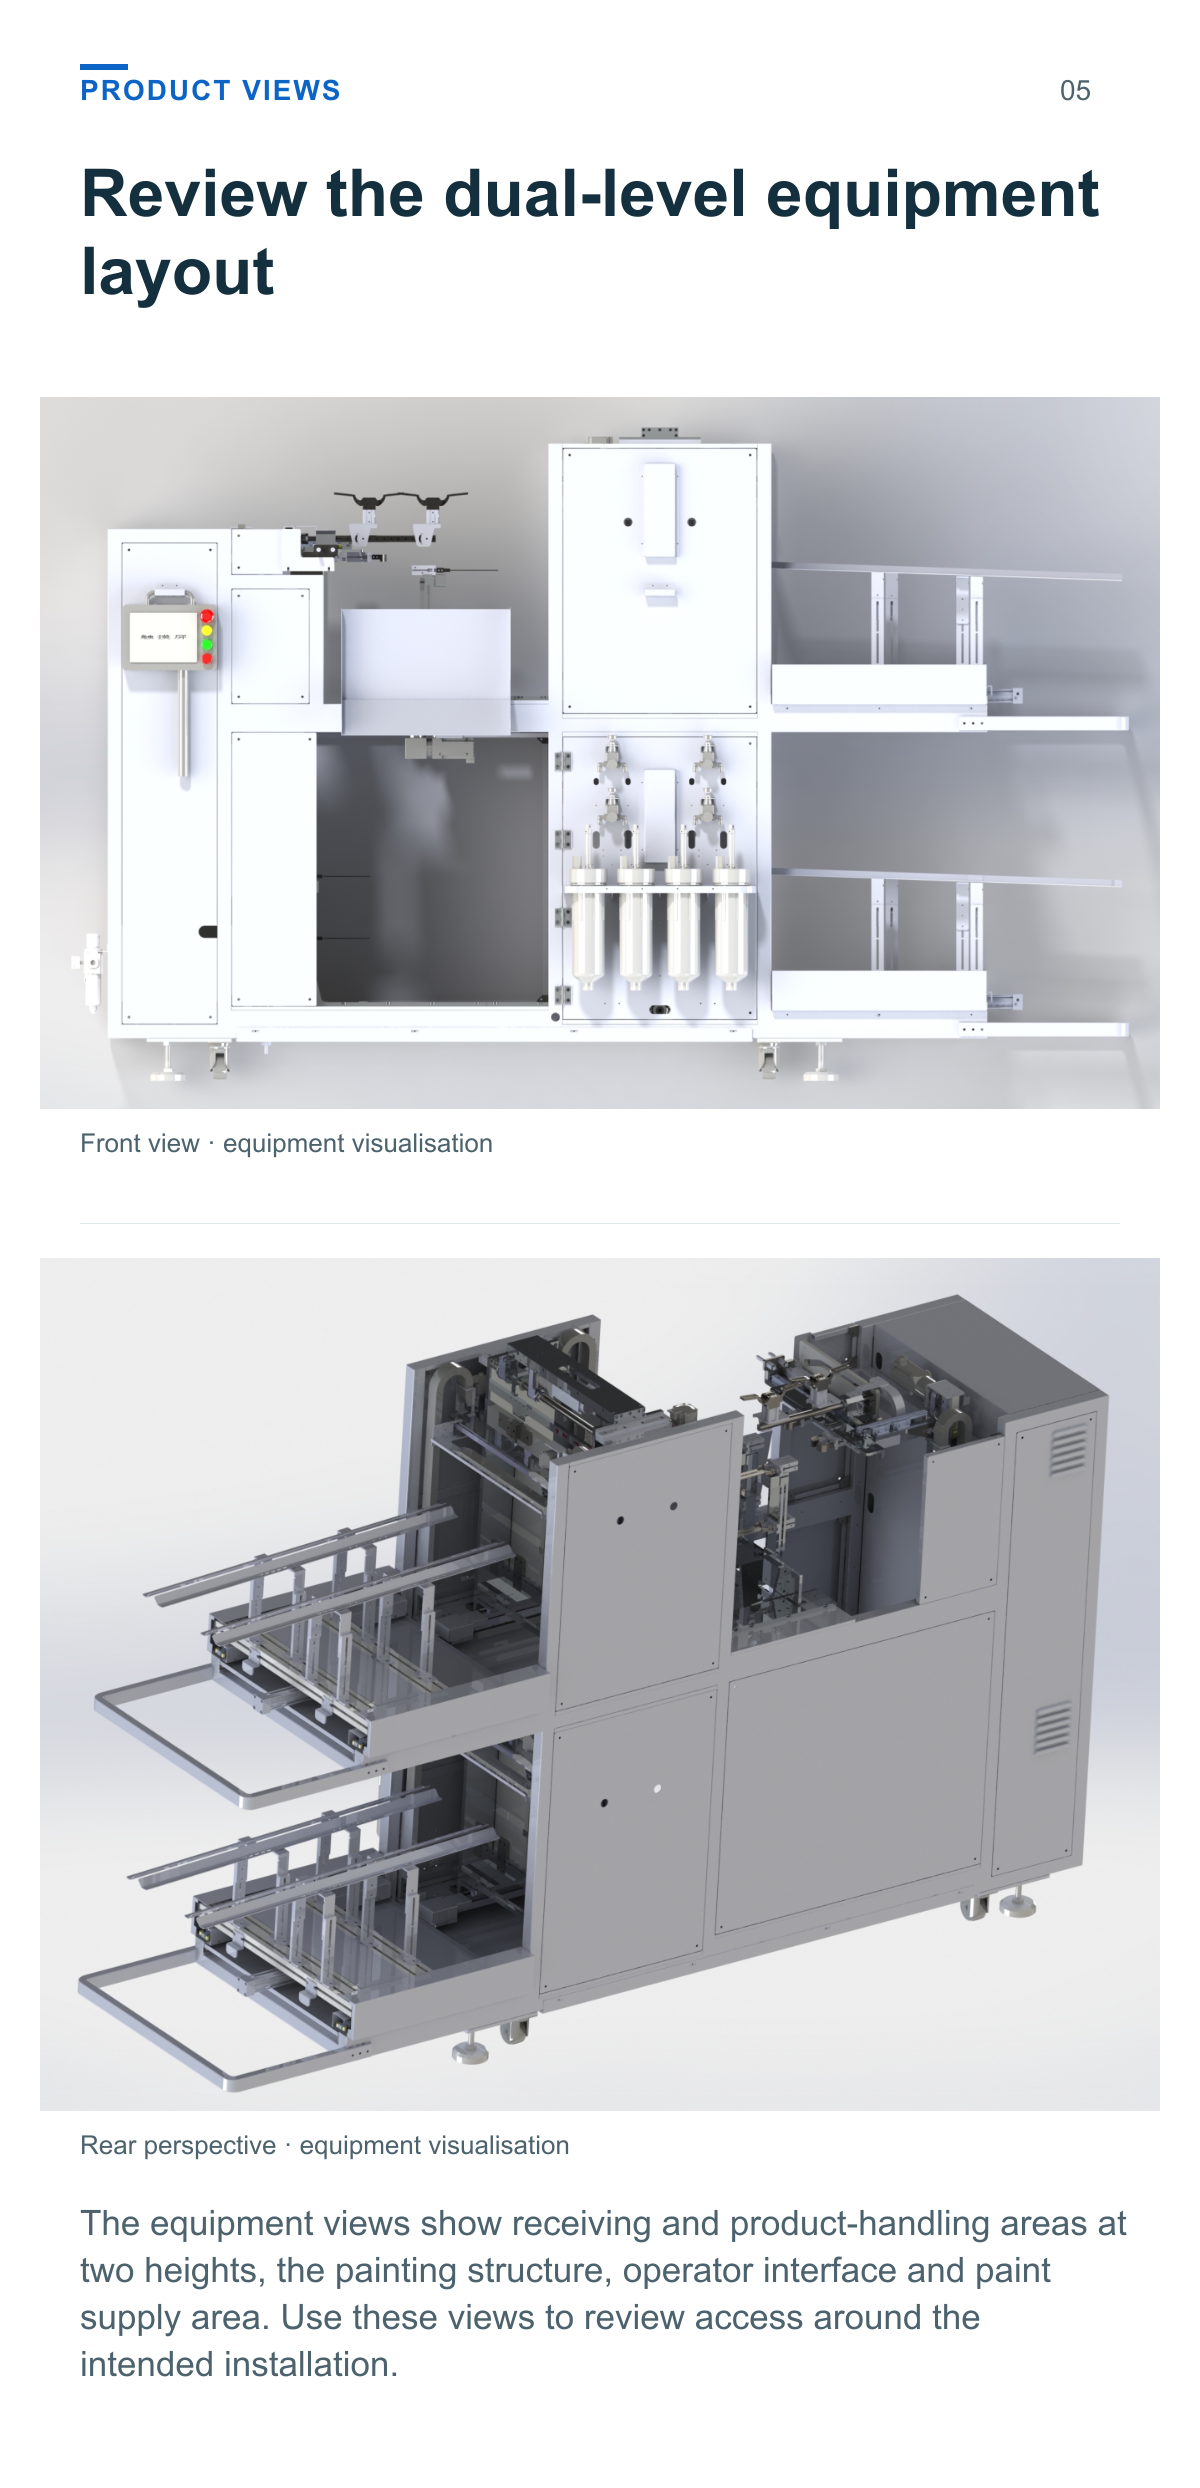
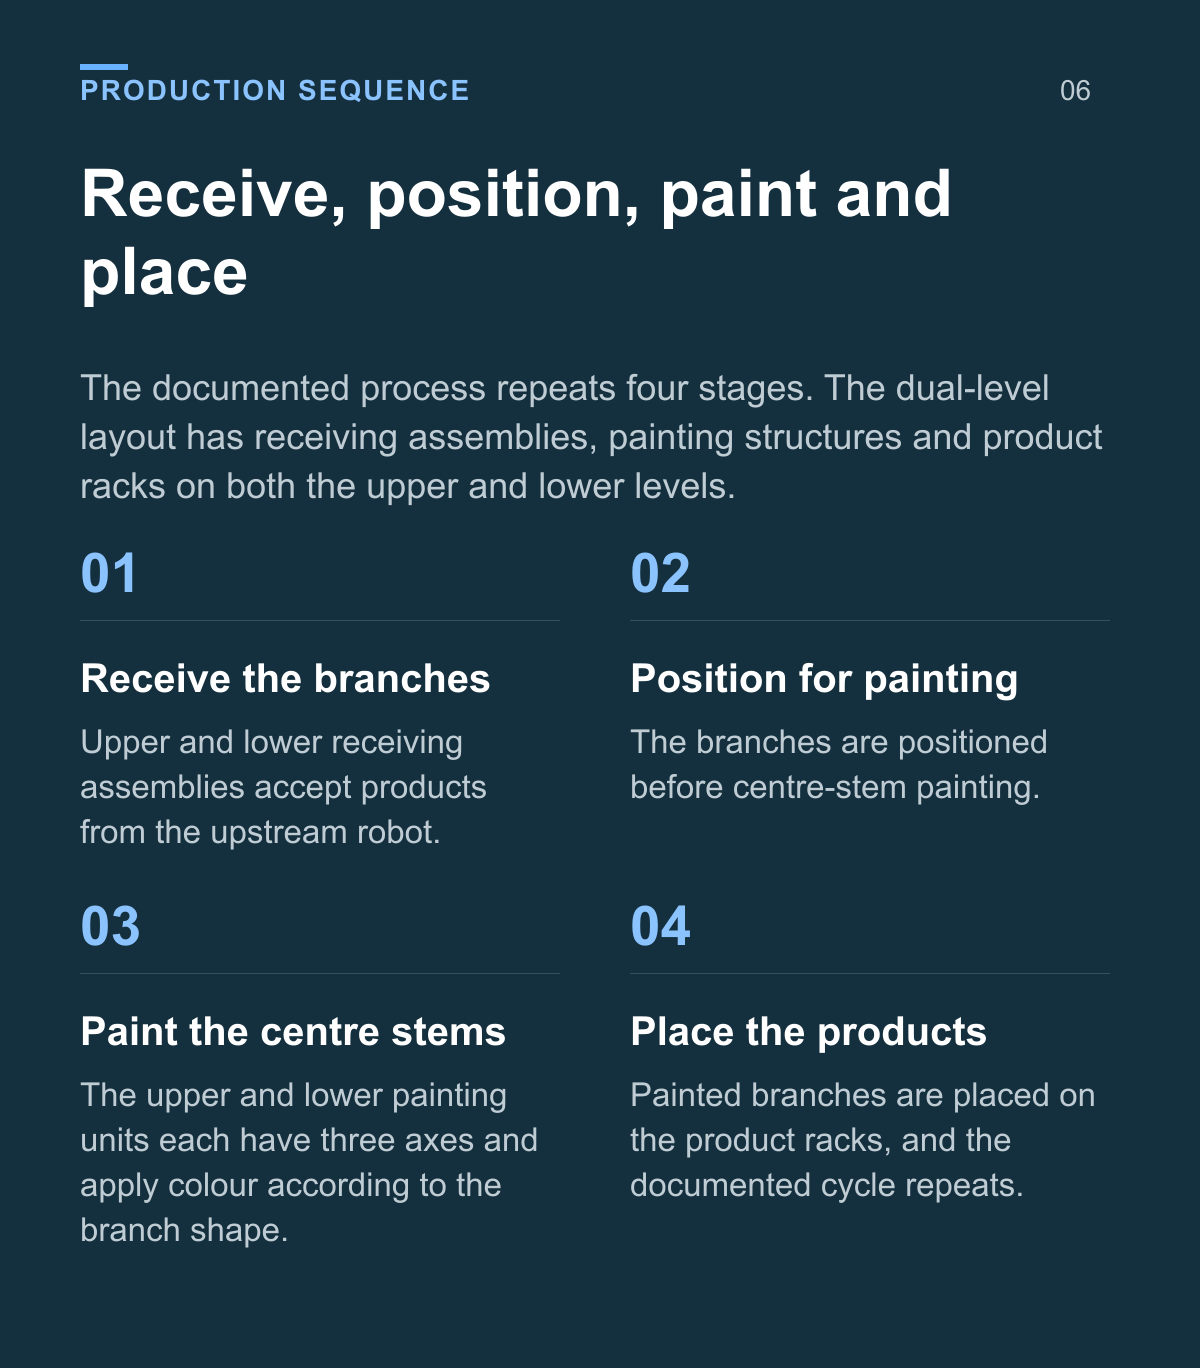
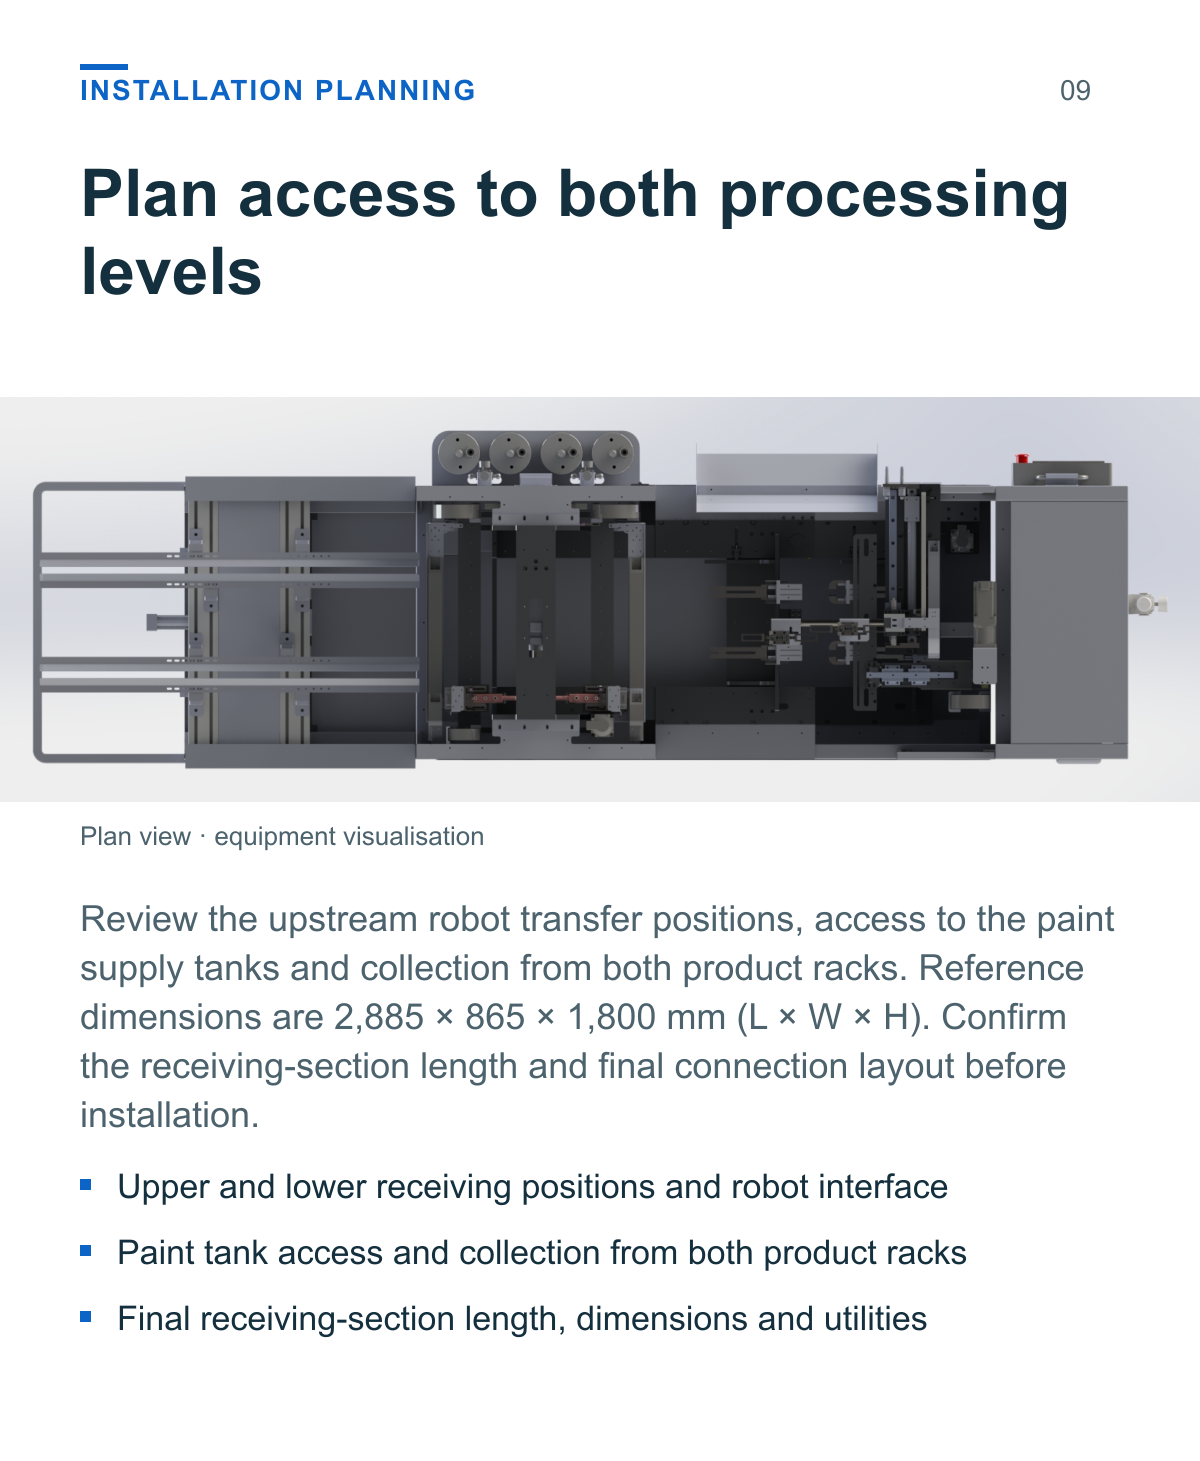
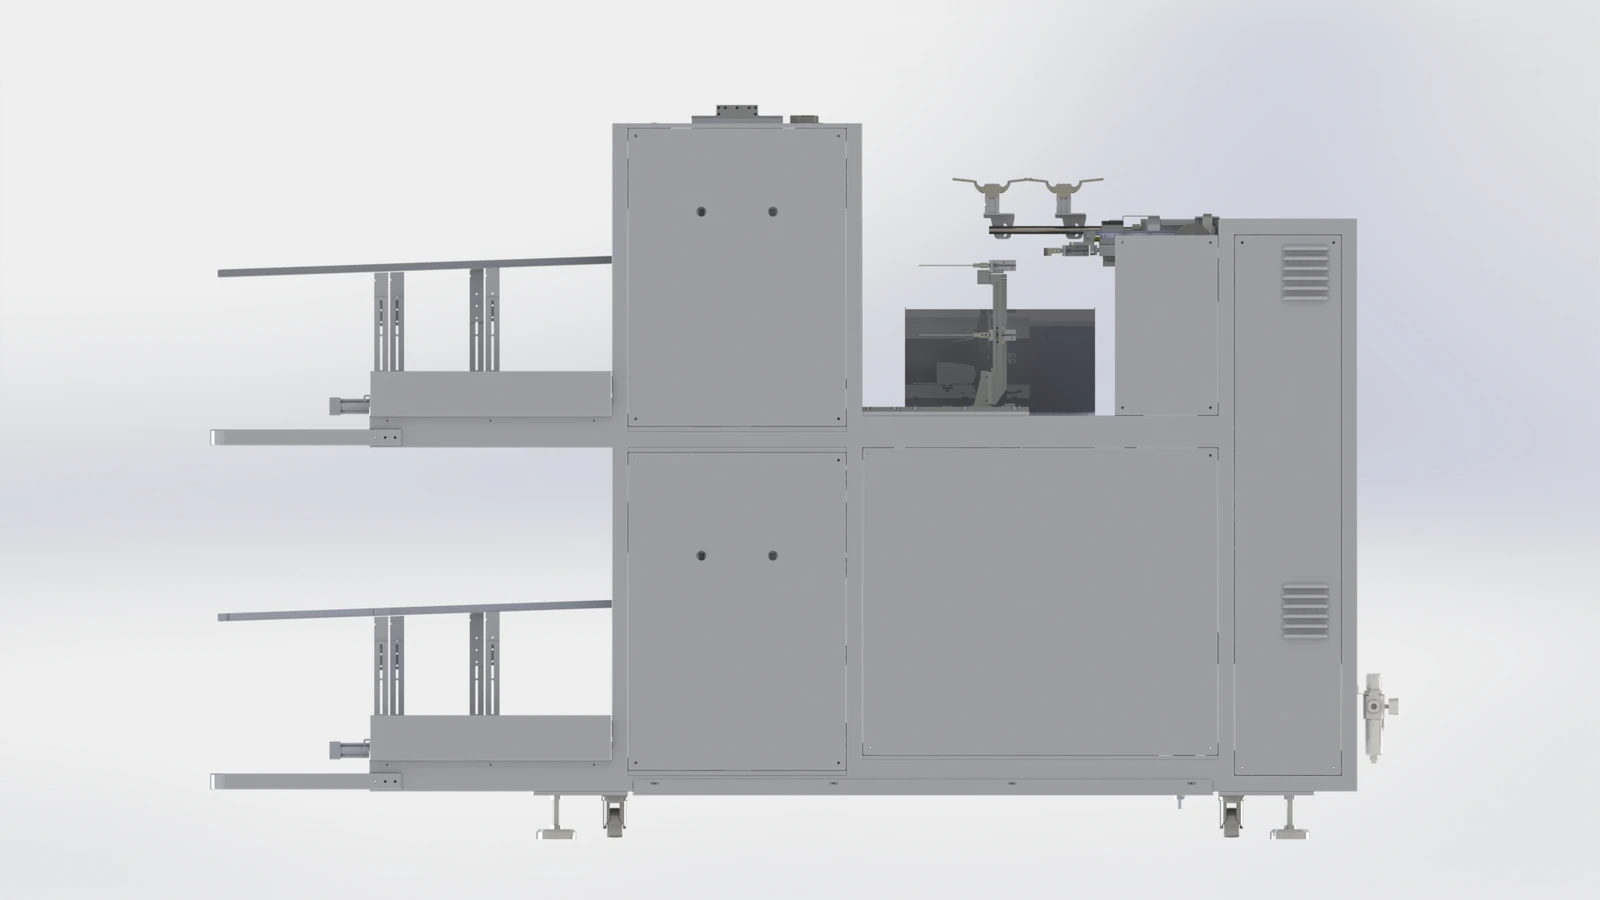
Review the dual level equipment layout
The equipment views show receiving and product-handling areas at two heights, the painting structure, operator interface and paint supply area. Use these views to review access around the intended installation.
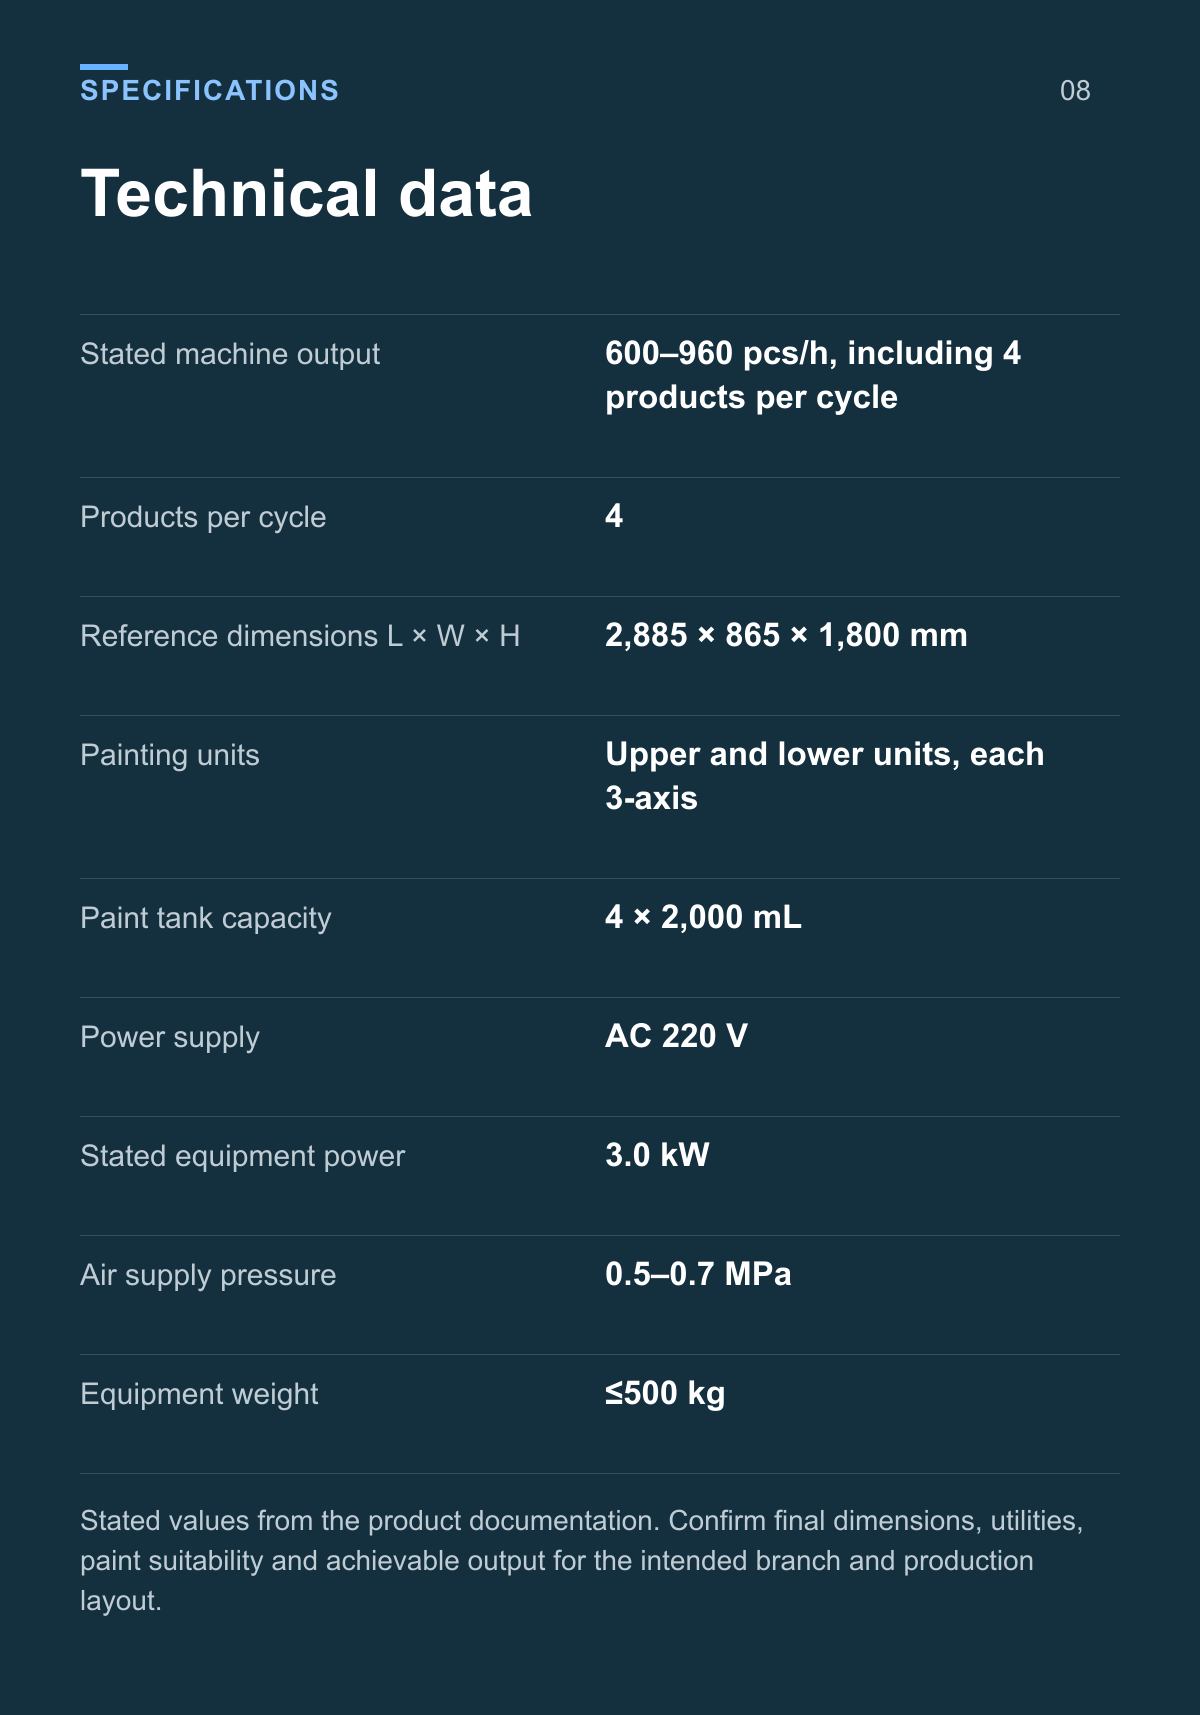
Technical data
| Parameter | Value |
|---|---|
| Stated machine output | 600–960 pcs/h, including 4 products per cycle |
| Products per cycle | 4 |
| Reference dimensions L × W × H | 2,885 × 865 × 1,800 mm |
| Painting units | Upper and lower units, each 3-axis |
| Paint tank capacity | 4 × 2,000 mL |
| Power supply | AC 220 V |
| Stated equipment power | 3.0 kW |
| Air supply pressure | 0.5–0.7 MPa |
| Equipment weight | ≤500 kg |
Stated values from the product documentation. Confirm final dimensions, utilities, paint suitability and achievable output for the intended branch and production layout.
Plan access to both processing levels
Review the upstream robot transfer positions, access to the paint supply tanks and collection from both product racks. Reference dimensions are 2,885 × 865 × 1,800 mm (L × W × H). Confirm the receiving-section length and final connection layout before installation.
- Upper and lower receiving positions and robot interface
- Paint tank access and collection from both product racks
- Final receiving-section length, dimensions and utilities
Assess the branch finish and transfer
Provide an unpainted branch and a reference for the required stem colour and finish. Review the branch geometry, painting path and presentation to the upper and lower receiving areas before confirming the setup.
Branch geometry
Provide the actual moulded branch and relevant dimensions.
Painted area and finish
Mark the centre-stem area to be painted and supply a colour or finished sample.
Paint and supply
Provide the paint specification and confirm the required supply arrangement.
Transfer and collection
State the robot transfer positions, hourly output target and collection method for both levels.
Application questions
What does the dual level layout include
The documented layout has upper and lower receiving assemblies, a three-axis painting structure on each level, and upper and lower product racks. Confirm the transfer arrangement for the intended branches.
Does the dual level layout multiply the stated output
No. The source states a machine output of 600–960 pcs/h for the four-output configuration. Use that range as the stated reference and confirm achievable output for the actual application.
Do four tanks provide four colour operation
Four 2,000 mL paint supply tanks are documented. Tank count alone does not establish simultaneous four-colour painting. Confirm the paint, colour requirement and supply arrangement for the intended finish.
What is needed for a painting assessment
Provide branch samples, the desired centre-stem colour and painted area, paint details, robot transfer positions and the hourly output target. Include the proposed collection method for both levels.
Define your dual level painting application
Provide the branch samples, target stem finish, paint specification, upstream robot arrangement and hourly output target to review the suitable dual-level painting setup.
Product views and application details